How to Fill Out Form QW-482

Form QW-482 at a glance

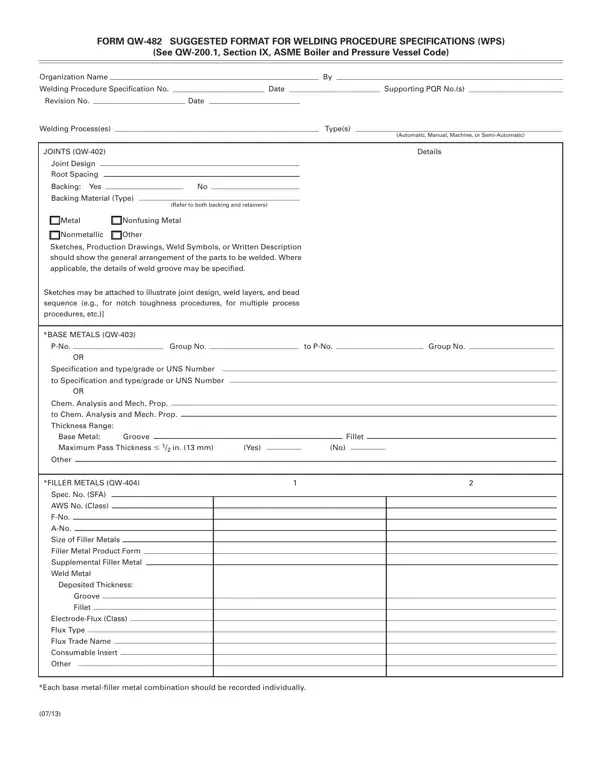
What it is: Form QW-482 is the suggested format for welding procedure specifications (WPS), see QW-200.1, Section IX, ASME Boiler and Pressure Vessel Code.

A filled-in Form QW-482 example: a welding procedure specification for one process
Form QW-482 example filled out, example: a welding procedure specification for one process
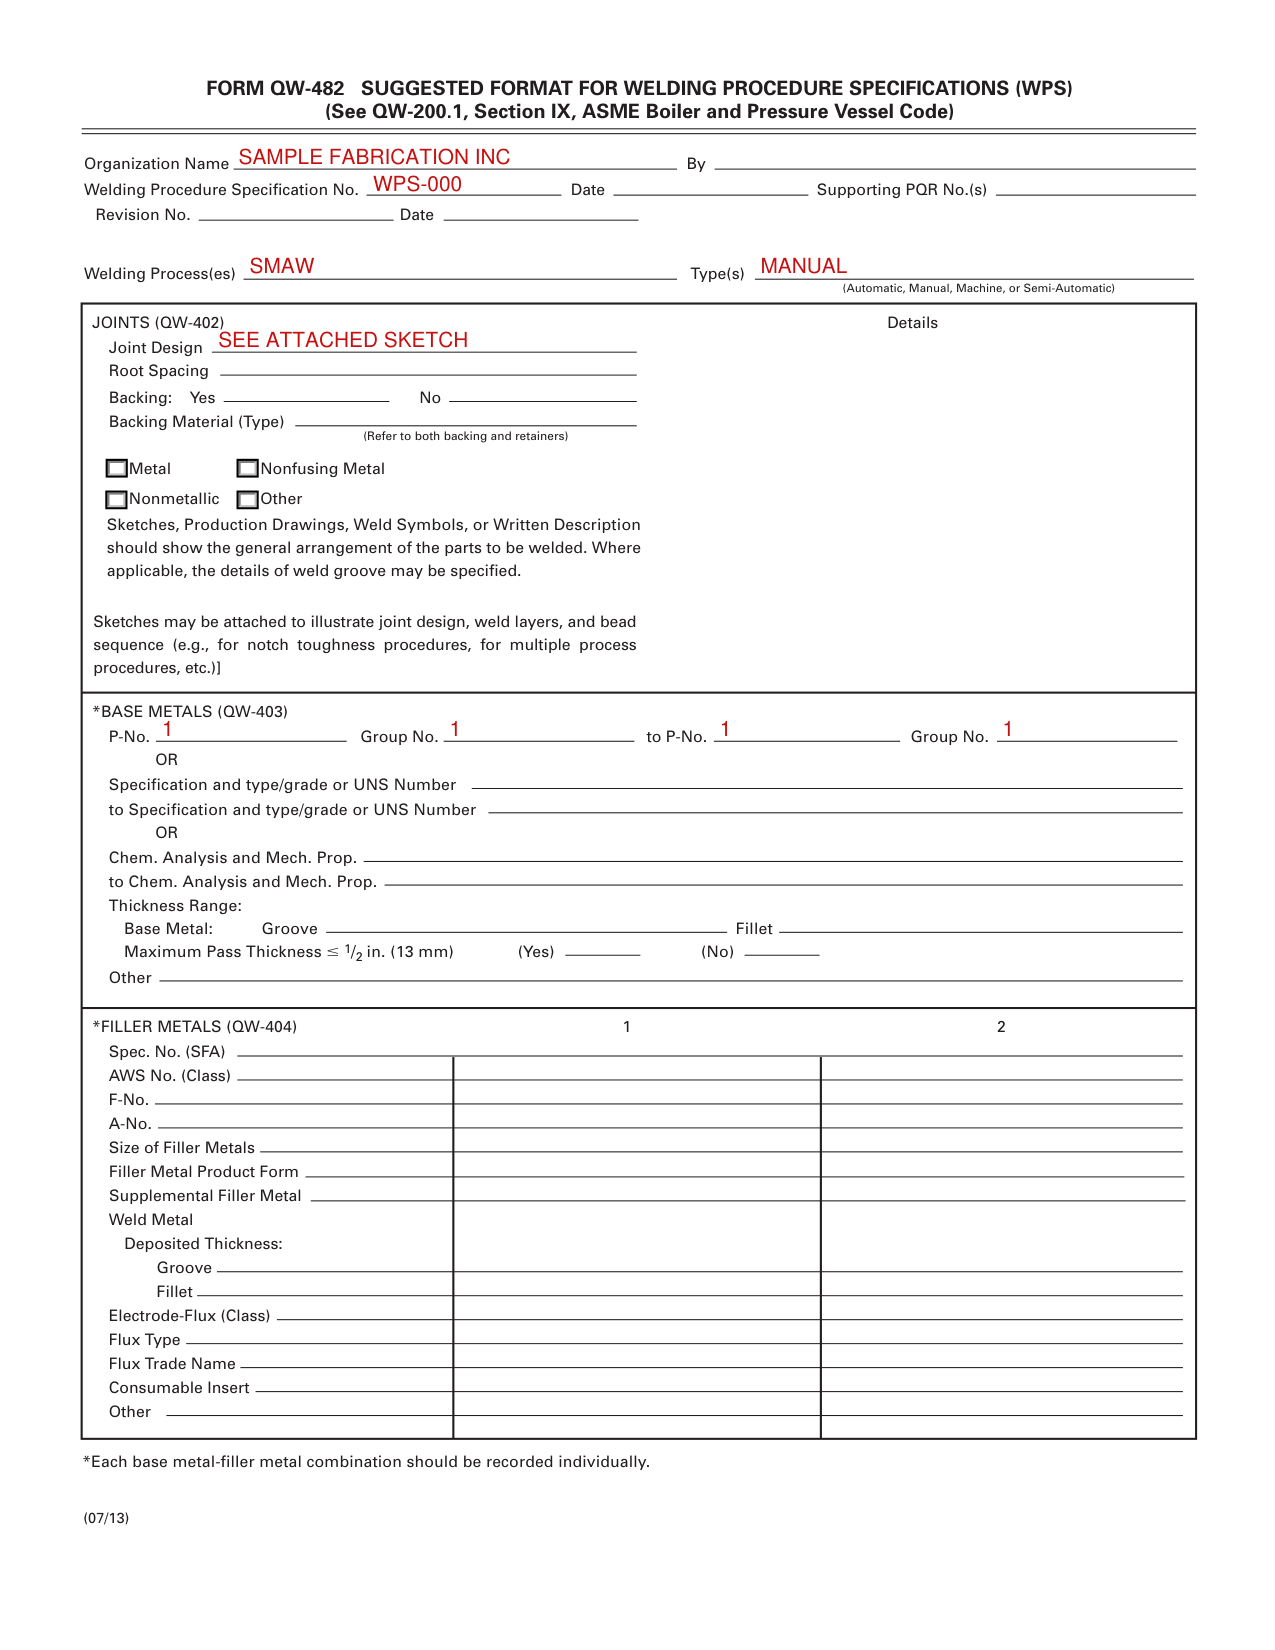
Sample Fabrication Inc. fills out Form QW-482 as a welding procedure specification. The procedure covers one process, SMAW, joining P-No. 1 base metal to P-No. 1 base metal. The picture shows the header and base metals; every value in it is made up. Joint Design points to an attached sketch.

How to fill out Form QW-482, box by box

Procedure and organization
Form QW-482 example filled out, procedure and organization

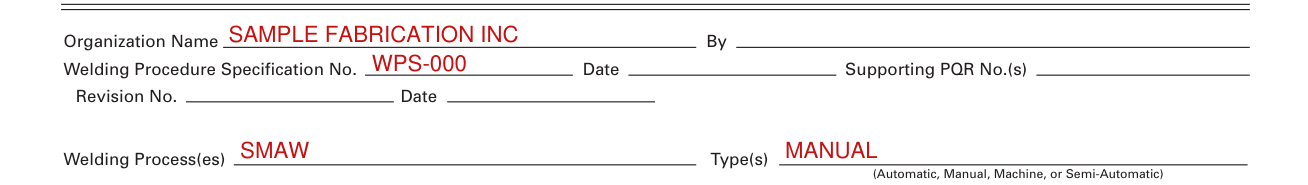
Enter the Organization Name.

Enter the Welding Procedure Specification No.

Enter the Welding Process(es) and the Type(s).

Type(s) are Automatic, Manual, Machine, or Semi-Automatic.

Joints
Form QW-482 example filled out, joints

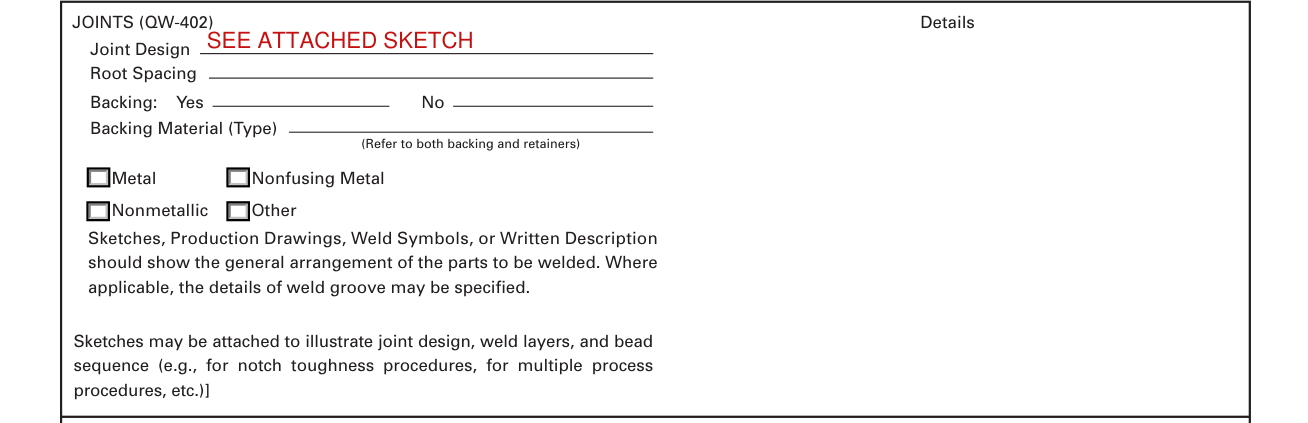
Sketches, Production Drawings, Weld Symbols, or Written Description should show the general arrangement of the parts to be welded.

Sketches may be attached to illustrate joint design, weld layers, and bead sequence.

Backing Material (Type) refers to both backing and retainers.

Base metals and filler metals
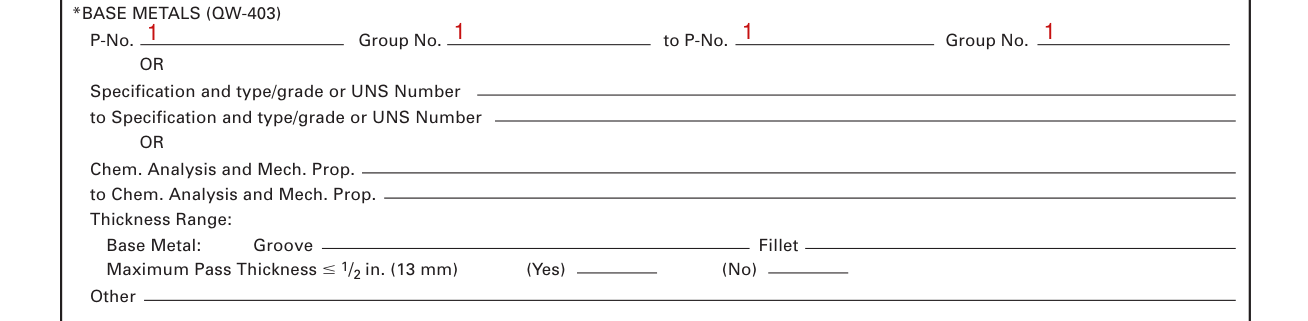
Form QW-482 example filled out, base metals and filler metals

Under BASE METALS (QW-403), enter the P-No. and Group No.

Each base metal-filler metal combination should be recorded individually.

Under FILLER METALS (QW-404), enter the Spec. No. (SFA) and the AWS No. (Class).

More rules for Form QW-482

Amps and volts, or power or energy range, should be recorded for each electrode size, position, and thickness, etc.

Continuous or special heating, where applicable, should be recorded.

Sources

[1] Form QW-482 (07/13), Suggested Format for Welding Procedure Specifications (WPS) (the Official source link on this page).

Form Wps Qw 482 PDF Details

In the realm of welding and fabrication, the formulation and adherence to detailed specifications play a pivotal role in ensuring the quality and safety of welded structures and components. Among the various documents that underpin this meticulous approach is the Wps Qw 482 form, a comprehensive guide recommended for outlining Welding Procedure Specifications (WPS) in accordance with QW-200.1, Section IX of the ASME Boiler and Pressure Vessel Code. This form, organized and used by entities engaging in welding activities, encompasses a wide array of technical details that welders and engineers must follow. From specifying the welding processes—whether automatic, manual, machine, or semi-automatic—to detailing the joints' design, including root spacing and whether backing is used, the form serves as a blueprint for welding operations. It further delves into the characteristics of base and filler metals, prescribing specifications, classes, and sizes, alongside the parameters for postweld heat treatment, gas composition, preheating requirements, and electrical characteristics relevant to the welding process. The intricacies extend to the welding technique itself, guiding on aspects such as bead type, cleaning methods, and electrode spacing. Through the encapsulation of these specifications, the Wps Qw 482 form stands as a critical document, ensuring that welding activities are performed within the bounds of safety, efficiency, and regulatory compliance.

QuestionAnswer
Form NameForm Wps Qw 482
Form Length2 pages
Fillable?No
Fillable fields0
Avg. time to fill out30 sec
Other namesform welding procedure wps, form welding procedure pdf, asme qw 482 form, format wps specification