
Form AB-76A at a glance
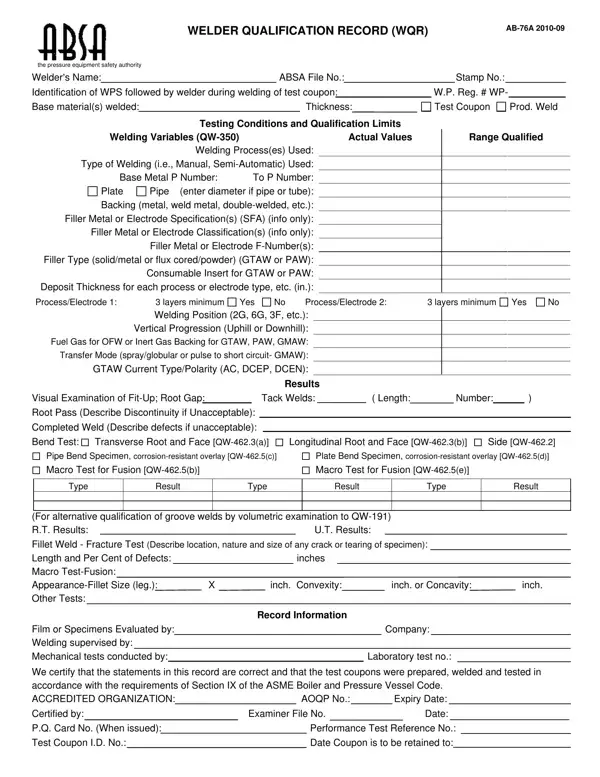
What it is: Welder Qualification Record (WQR) AB-76A 2010-09.
Who signs: If an accredited organization certifies the record, enter Certified by, Examiner File No. and Date under ACCREDITED ORGANIZATION.
A filled-in Form AB-76A example: a welder records a plate test
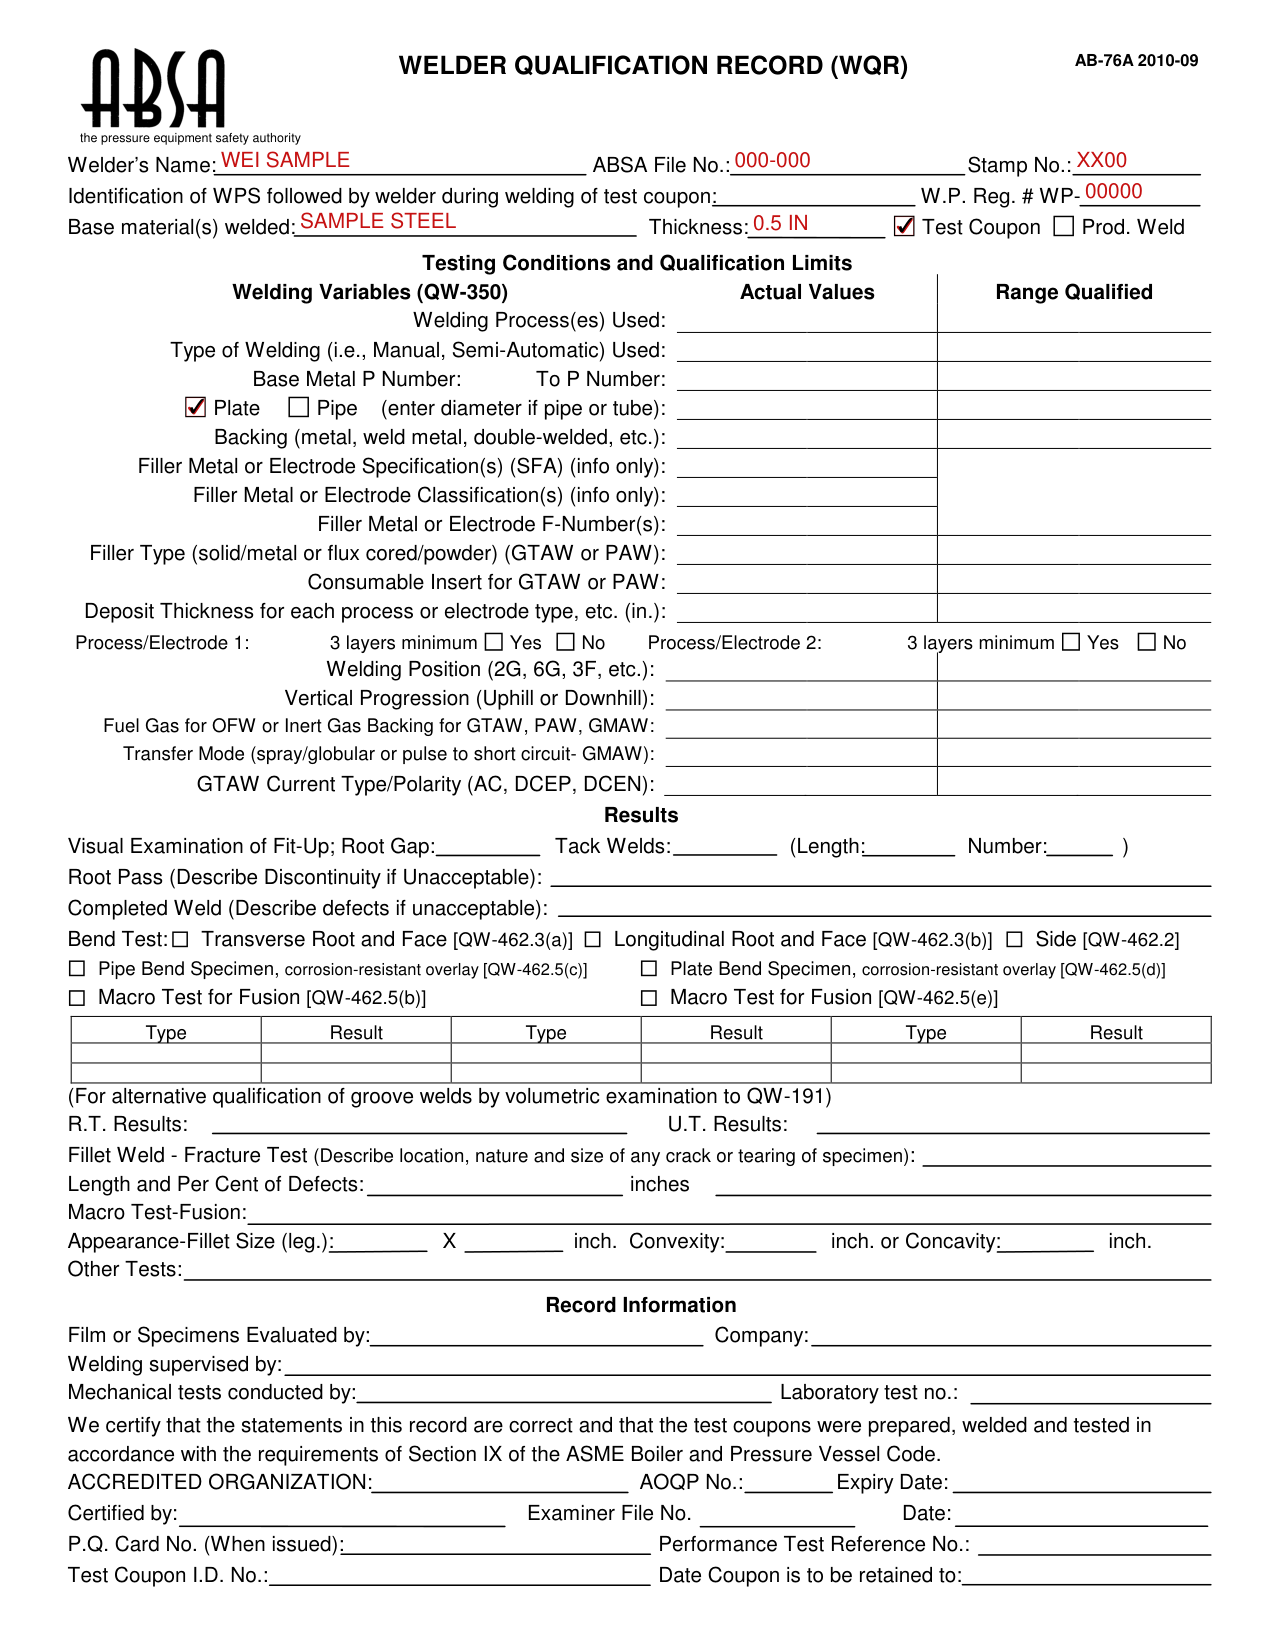
How to fill out Form AB-76A, box by box
Welder and test coupon
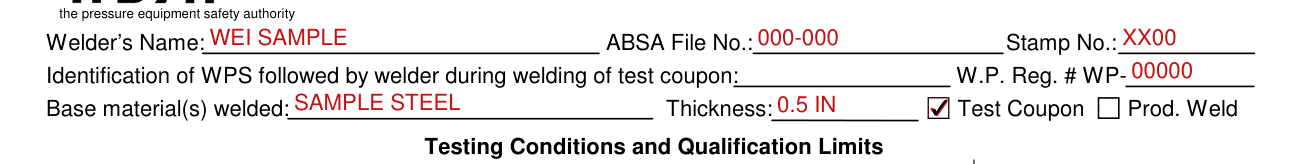
Enter the Welder's Name, ABSA File No., Stamp No., Identification of WPS followed by welder during welding of test coupon, W.P. Reg. # WP- and Base material(s) welded, then the Thickness and mark Test Coupon or Prod. Weld.
Testing conditions and qualification limits
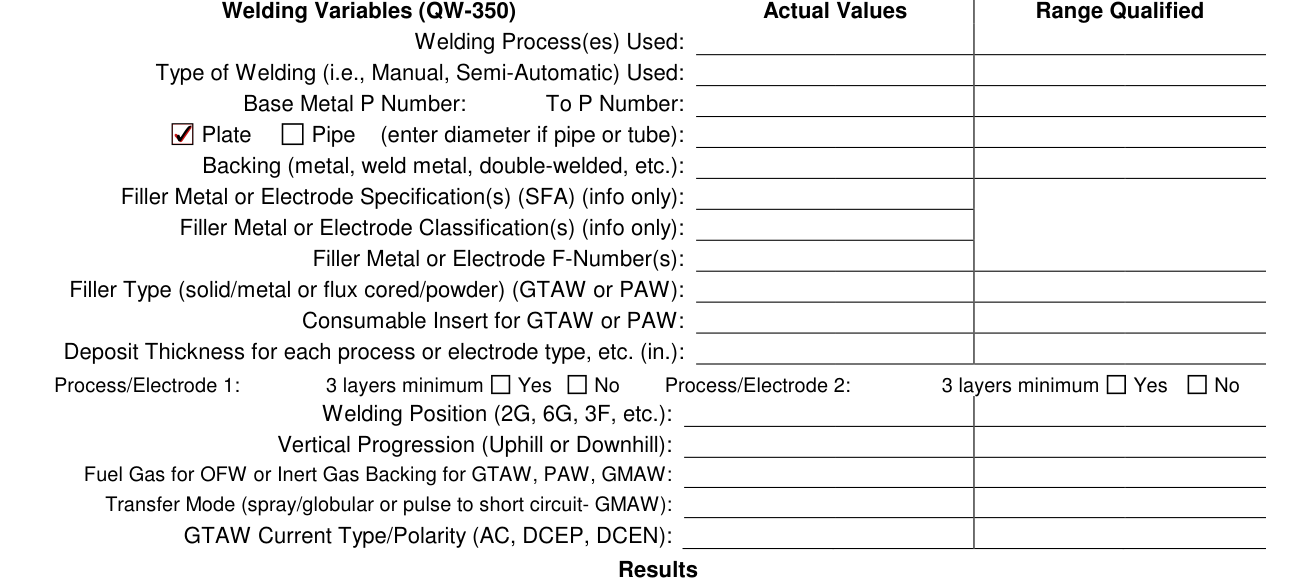
Under Testing Conditions and Qualification Limits, Welding Variables (QW-350), enter the Actual Values and the Range Qualified for Welding Process(es) Used and Type of Welding (i.e., Manual, Semi-Automatic) Used.
Enter the Base Metal P Number and ToP Number, mark Plate or Pipe (enter diameter if pipe or tube), and enter Backing (metal, weld metal, double-welded, etc.) and Filler Metal or Electrode Specification(s) (SFA) (info only).
Enter Filler Metal or Electrode Classification(s) (info only).
Enter Filler Metal or Electrode F-Number(s) and Filler Type (solid/metal or flux cored/powder) (GTAW or PAW).
Enter Consumable Insert for GTAW or PAW and Deposit Thickness for each process or electrode type, etc. (in.).
For Process/Electrode 1 and Process/Electrode 2, mark Yes or No for 3 layers minimum, then enter Welding Position (2G, 6G, 3F, etc.), Vertical Progression (Uphill or Downhill) and Fuel Gas for OFW or Inert Gas Backing for GTAW, PAW, GMAW.
Enter Transfer Mode (spray/globular or pulse to short circuit GMAW).
Enter GTAW Current Type/Polarity (AC, DCEP, DCEN).
Results
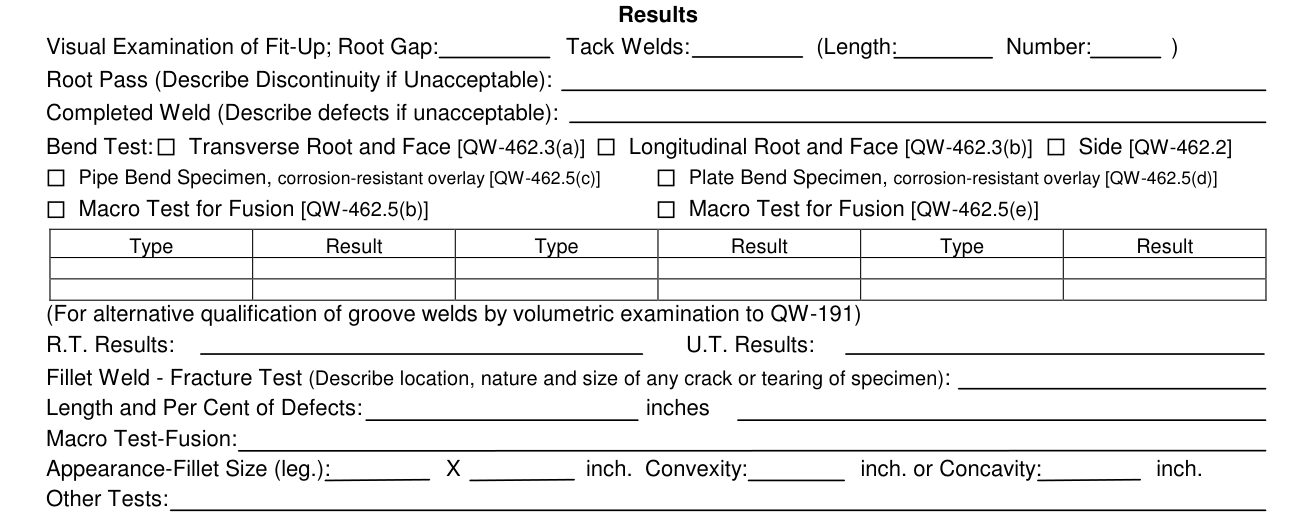
Under Results, enter Visual Examination of Fit-Up; Root Gap, Tack Welds (Length: Number: ), Root Pass (Describe Discontinuity if Unacceptable) and Completed Weld (Describe defects if unacceptable). Then mark the Bend Test: Transverse Root and Face [QW-462.3(a)]. Or mark Longitudinal Root and Face [QW-462.3(b)], Side [QW-462.2]. Or mark Pipe Bend Specimen, corrosion-resistant overlay [QW-462.5(c)]. Or mark Plate Bend Specimen, corrosion-resistant overlay [QW-462.5(d)]. Or mark Macro Test for Fusion [QW-462.5(b)] or Macro Test for Fusion [QW-462.5(e)].
Enter each Type and Result.
For alternative qualification of groove welds by volumetric examination to QW-191, enter R.T. Results and U.T. Results. For the Fillet Weld - Fracture Test, enter Describe location, nature and size of any crack or tearing of specimen and the Length and Per Cent of Defects: inches. Enter Macro Test-Fusion, Appearance-Fillet Size (leg.): X inch. Convexity: inch. or Concavity: inch. and Other Tests.
Record information

Under Record Information, enter Film or Specimens Evaluated by, Company, Welding supervised by, Mechanical tests conducted by and Laboratory test no.
Certification
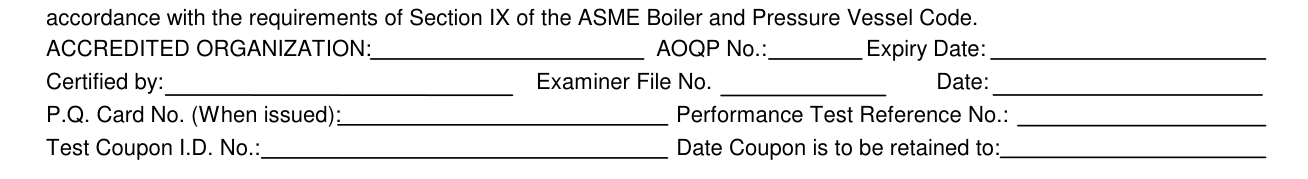
If an accredited organization certifies the record, it certifies that the statements in this record are correct and that the test coupons were prepared, welded and tested in accordance with the requirements of Section IX of the ASME Boiler and Pressure Vessel Code, and enters ACCREDITED ORGANIZATION, AOQP No., Expiry Date, P.Q. Card No. (When issued), Performance Test Reference No., Test Coupon I.D. No. and Date Coupon is to be retained to.
If an accredited organization certifies the record, enter Certified by, Examiner File No. and Date under ACCREDITED ORGANIZATION.
Sources
[1] Form AB-76A (2010-09), Welder Qualification Record (WQR), the pressure equipment safety authority (the Official source link on this page).