

Form QW-484A at a glance
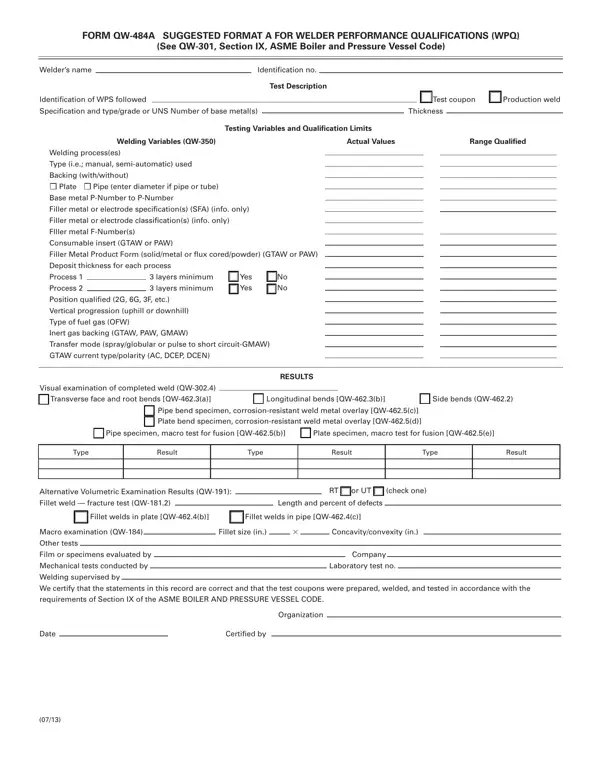
What it is: Form QW-484A Suggested Format A for Welder Performance Qualifications (WPQ) (See QW-301, Section IX, ASME Boiler and Pressure Vessel Code).
Who signs: Enter the Organization, SIGN as Certified by and enter the Date.
A filled-in Form QW-484A example: a welder's record is certified
How to fill out Form QW-484A, box by box
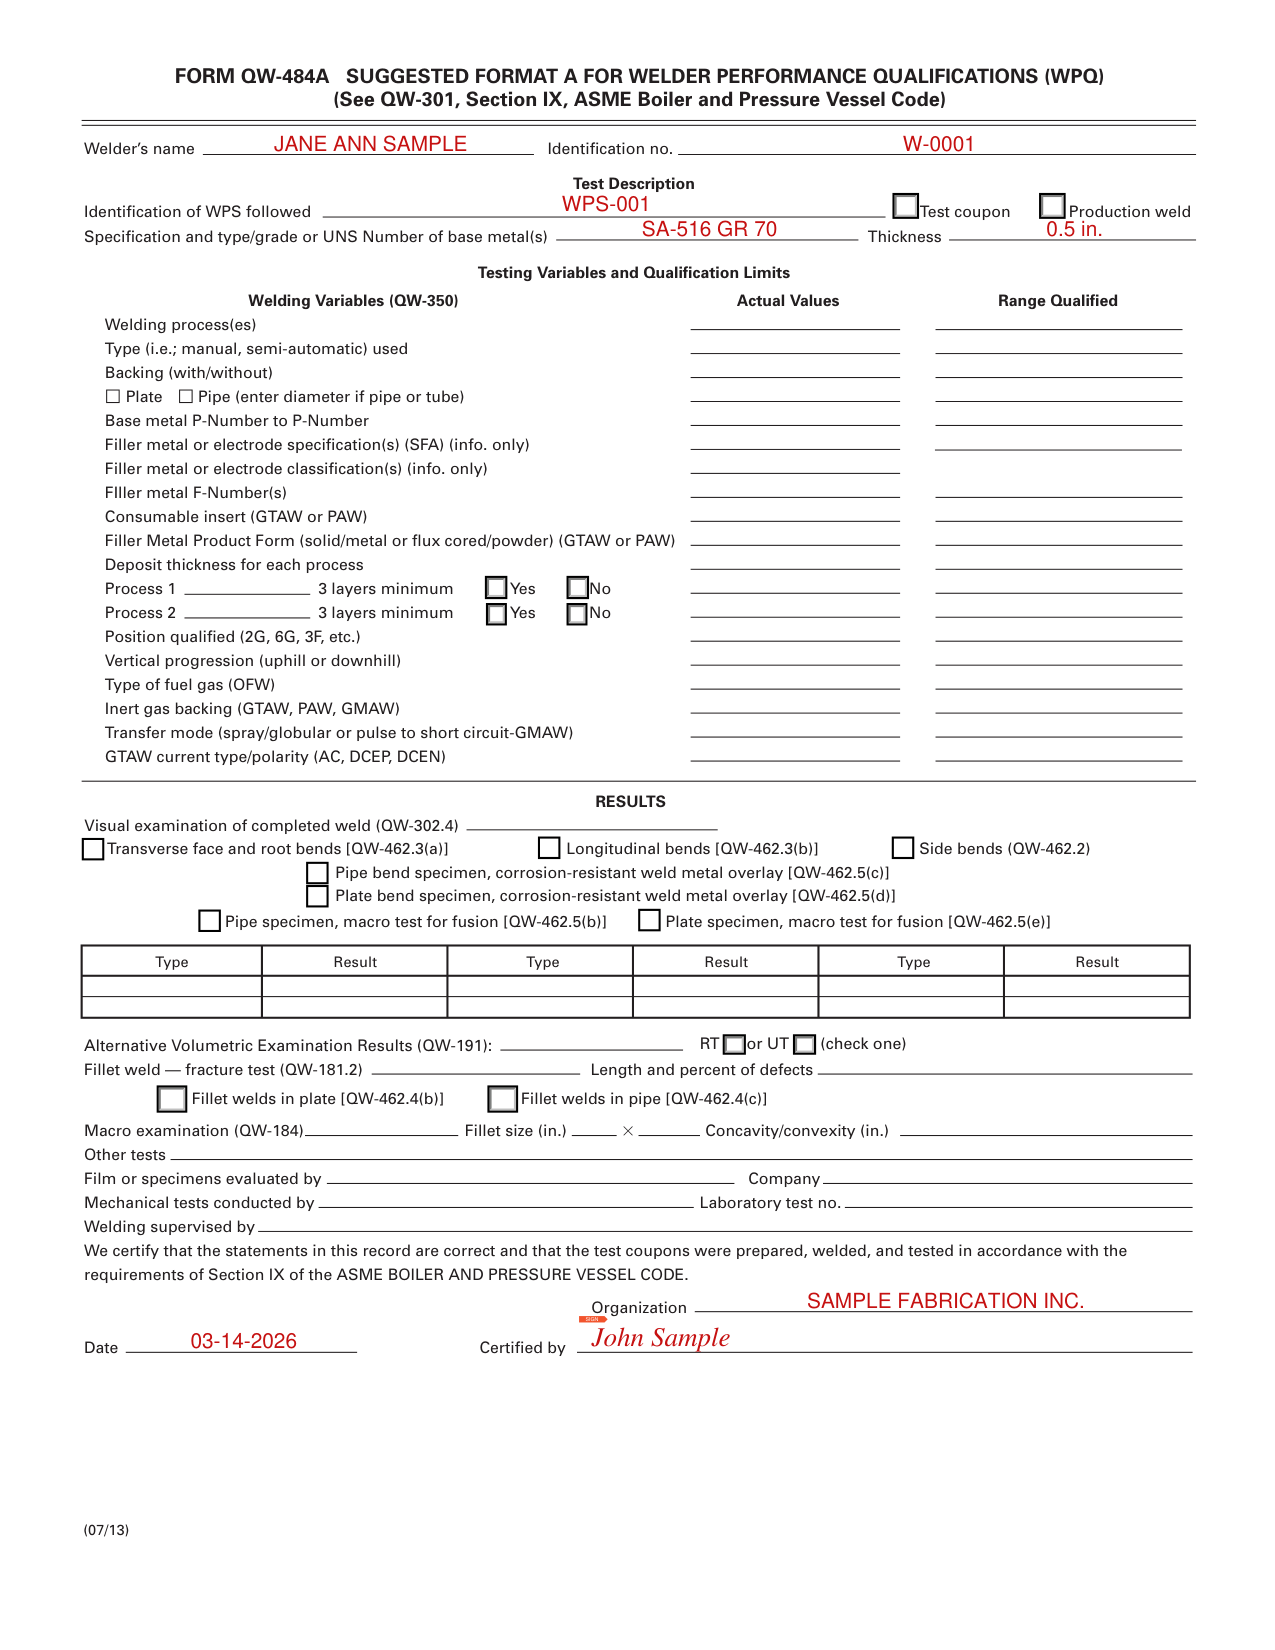
Welder's name and Identification no.

Enter the Welder's name and the Identification no.
Test Description and Thickness

Under Test Description, enter the Identification of WPS followed and the Specification and type/grade or UNS Number of base metal(s).
Enter the Thickness of the Test coupon or Production weld.
Testing Variables and Qualification Limits
Under Testing Variables and Qualification Limits, enter the Actual Values for the Welding Variables (QW-350) and the Range Qualified.
Fill in the Welding process(es), the Type (i.e.; manual, semi-automatic) used, the Backing (with/without), the Plate or Pipe (enter diameter if pipe or tube) and the Base metal P-Number to P-Number.
Fill in the Filler metal or electrode specification(s) (SFA) (info. only), the Filler metal or electrode classification(s) (info. only), the Filler metal F-Number(s), the Consumable insert (GTAW or PAW) and the Filler Metal Product Form (solid/metal or flux cored/powder) (GTAW or PAW).
Deposit thickness for each process
For the Deposit thickness for each process, fill in Process 1 and Process 2 and mark Yes or No for 3 layers minimum.
Position qualified, gas and current
Fill in the Position qualified (2G, 6G, 3F, etc.), the Vertical progression (uphill or downhill), the Type of fuel gas (OFW), the Inert gas backing (GTAW, PAW, GMAW), the Transfer mode (spray/globular or pulse to short circuit-GMAW) and the GTAW current type/polarity (AC, DCEP, DCEN).
RESULTS
Under RESULTS, enter the Visual examination of completed weld (QW-302.4).
Enter the Type and Result of the Transverse face and root bends [QW-462.3(a)], Longitudinal bends [QW-462.3(b)], Side bends (QW-462.2), Pipe bend specimen, corrosion-resistant weld metal overlay [QW-462.5(c)], Plate bend specimen, corrosion-resistant weld metal overlay [QW-462.5(d)], Pipe specimen, macro test for fusion [QW-462.5(b)] and Plate specimen, macro test for fusion [QW-462.5(e)].
Alternative Volumetric Examination Results and Macro examination
For the Alternative Volumetric Examination Results (QW-191), enter the result and mark RT or UT (check one). Enter the Fillet weld - fracture test (QW-181.2) Length and percent of defects.
Mark Fillet welds in plate [QW-462.4(b)] or Fillet welds in pipe [QW-462.4(c)], then enter the Macro examination (QW-184), the Fillet size (in.) and the Concavity/convexity (in.).
Other tests and Welding supervised by
Under Other tests, enter the Film or specimens evaluated by, the Company, the Mechanical tests conducted by, the Laboratory test no. and Welding supervised by.
Certification
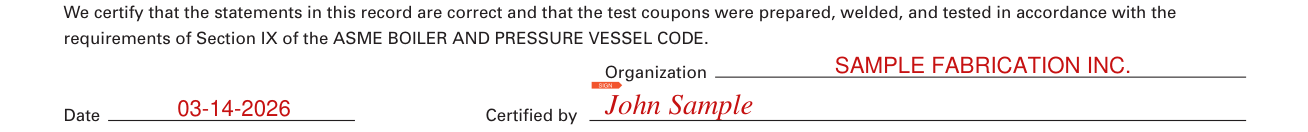
Certify that the statements in this record are correct and that the test coupons were prepared, welded, and tested in accordance with the requirements of Section IX of the ASME BOILER AND PRESSURE VESSEL CODE.
Sources
[1] Form QW-484A Suggested Format A for Welder Performance Qualifications (WPQ) (07/13), ASME Boiler and Pressure Vessel Code, Section IX (the Official source link on this page).