Welder Performance Qualification Record PDF Details

Within the realm of professional welding, the documentation of a welder's skill and compliance with industry standards plays a crucial role in maintaining the integrity and safety of welded structures. The Welder Performance Qualification Record form serves as a fundamental piece of this documentation puzzle, offering a comprehensive overview of a welder's capabilities and the specific conditions under which they were tested. This form captures vital information such as the welder's name, social security number, test parameters, and the welding processes used, ranging from manual to automatic. It details not only the equipment and materials employed—like base metals, filler metals, and shielding gases—but also the dimensions of the welds produced and the techniques applied. Further, it records both mechanical test results and nondestructive examination findings, providing a clear and thorough account of a welder's proficiency. As such, the Welder Performance Qualification Record is an indispensable tool for verifying that the welds carried out on a project meet the rigorous standards set by codes such as those from the American Welding Society, ensuring the safety and reliability of welding work.

QuestionAnswer
Form NameWelder Performance Qualification Record
Form Length1 pages
Fillable?No
Fillable fields0
Avg. time to fill out15 sec
Other nameswelder performance qualification, welders qualification test certificate, welding certificate format, welder format record

How to Fill Out Welder and Welding Operator Performance Qualification Record

Welder and Welding Operator Performance Qualification Record at a glance

What it is: The Welder and Welding Operator Performance Qualification Record has a Qualification Test Detail, a Qualification Range, Mechanical Test Results and Nondestructive Examination Results.

Who signs: Sign on Signed By with the CWI No., and enter the Date Qualified and the ATF Name and Number.

A filled-in Welder and Welding Operator Performance Qualification Record example: an inspector records a manual groove weld test
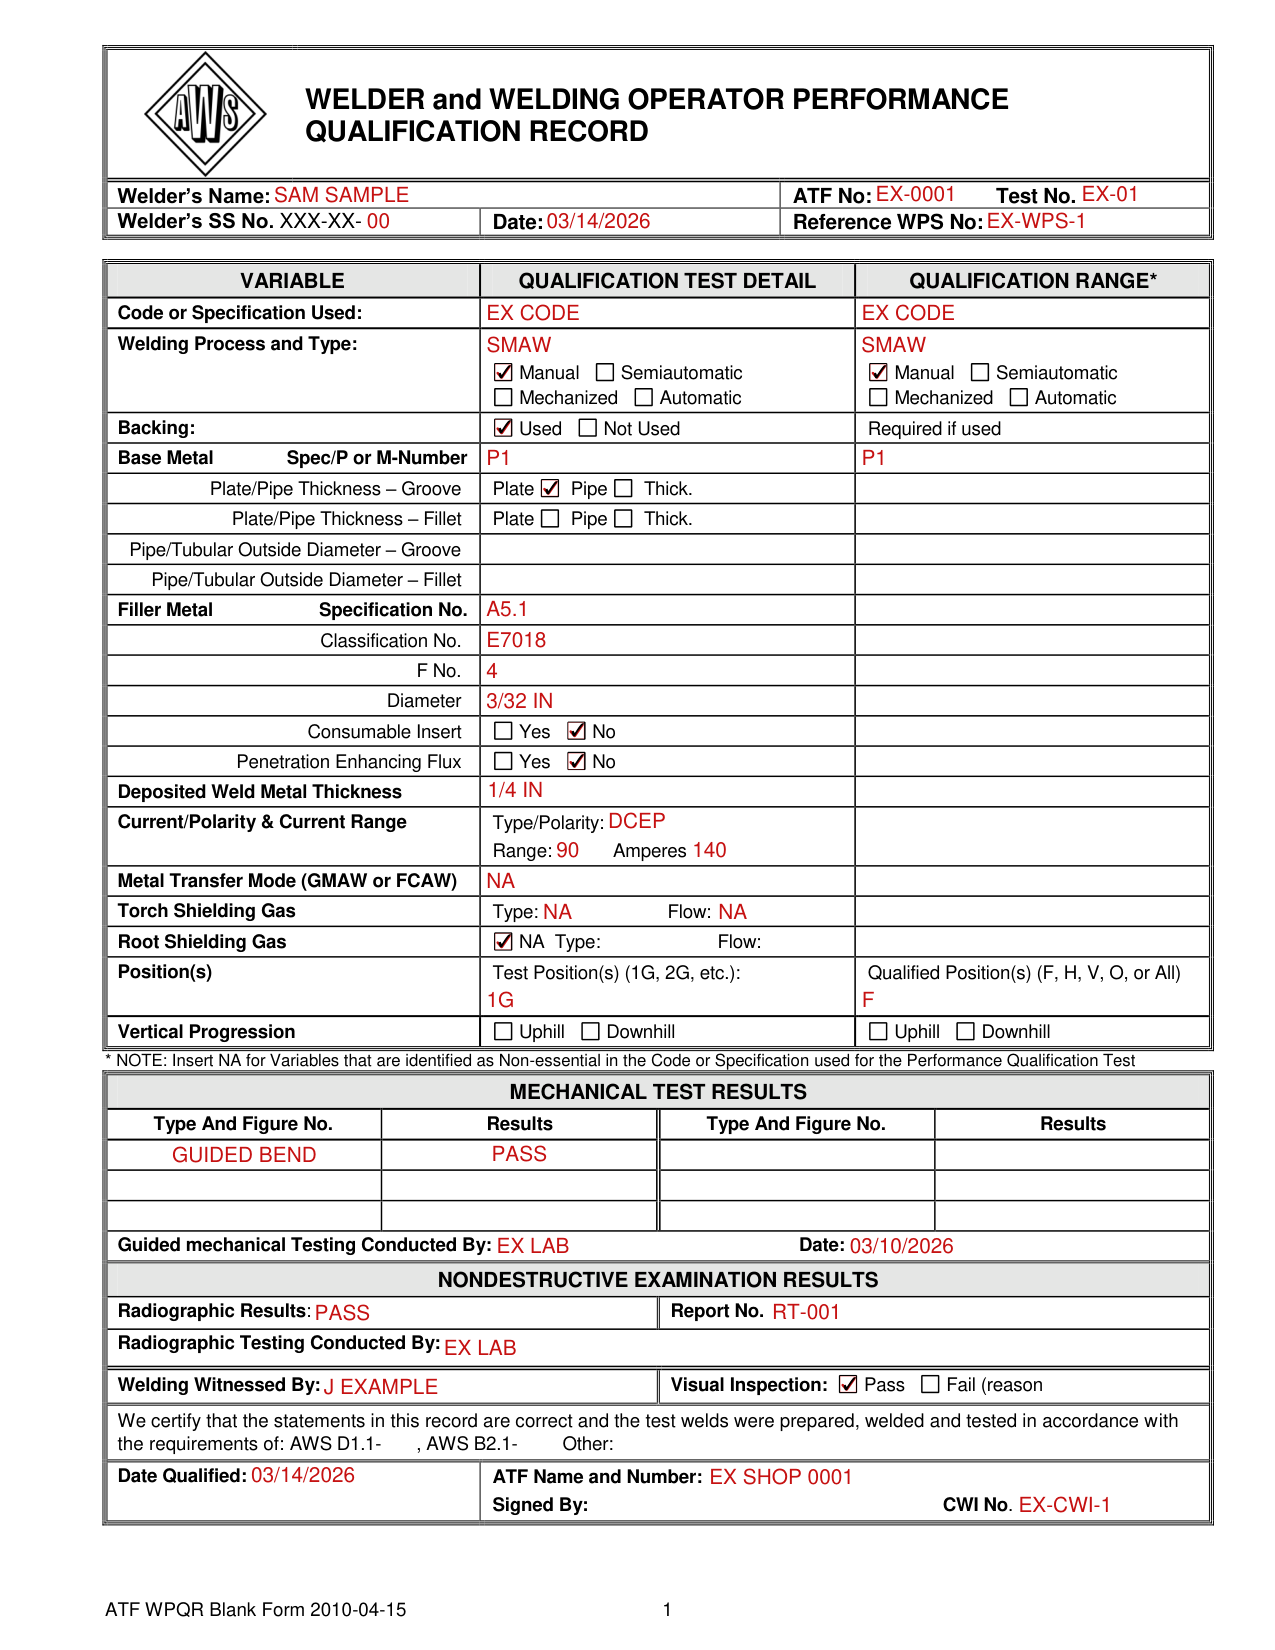
Welder and Welding Operator Performance Qualification Record example filled out, example: an inspector records a manual groove weld test
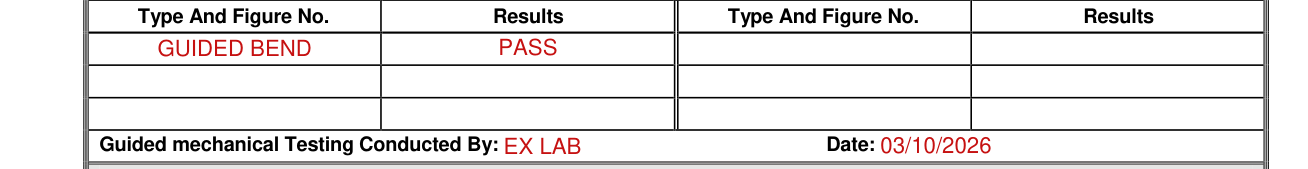
Sam Sample, an inspector, records one manual groove weld test on plate. It is a flat position test with no root shielding gas, so vertical progression stays empty. The picture shows page 1 only; none of its entries is real. A backing is used, so Used is marked and Not Used stays empty. The weld has no consumable insert and no penetration enhancing flux, so No is marked for both. The test is on plate, so nothing goes in Pipe/Tubular Outside Diameter because no pipe is welded. One guided bend test is recorded, so the later result rows stay empty. The Qualification Range column keeps only the code, process and base metal because the range is set later.

How to fill out Welder and Welding Operator Performance Qualification Record, box by box

Welder, test and reference

Welder and Welding Operator Performance Qualification Record example filled out, welder, test and reference

Enter the Welder's Name, ATF No, Test No., Welder's SS No. XXX-XX-, Date and Reference WPS No.

Code, specification and welding process
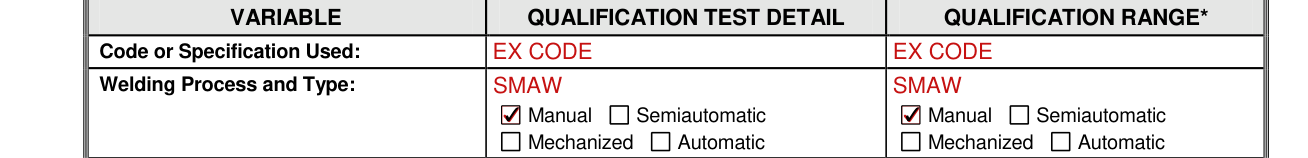
Welder and Welding Operator Performance Qualification Record example filled out, code, specification and welding process

Under Qualification Test Detail and under Qualification Range, enter the Code or Specification Used and the Welding Process and Type, and mark Manual, Semiautomatic, Mechanized or Automatic.

Backing, base metal and thickness

Welder and Welding Operator Performance Qualification Record example filled out, backing, base metal and thickness

For Backing, mark Used or Not Used, and use the Required if used boxes.

Enter the Base Metal Spec/P or M-Number, and the Plate/Pipe Thickness for Groove and for Fillet, marking Plate or Pipe.

Diameter, filler metal and flux
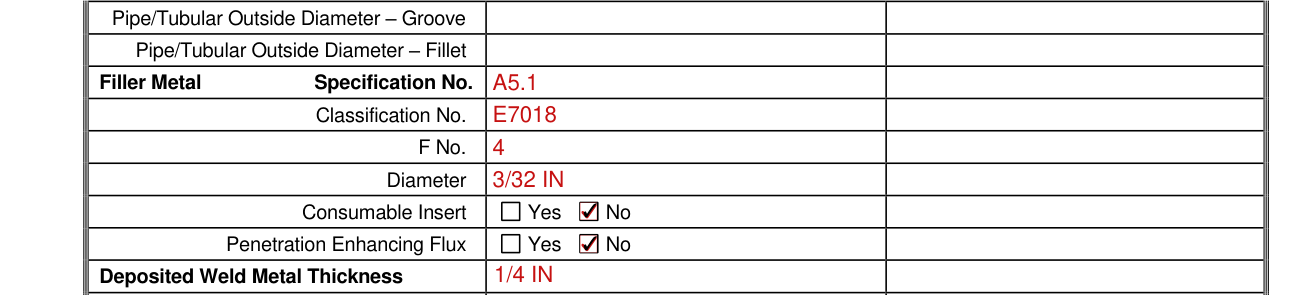
Welder and Welding Operator Performance Qualification Record example filled out, diameter, filler metal and flux

Enter the Pipe/Tubular Outside Diameter for Groove and for Fillet.

Enter the Filler Metal Specification No., Classification No., F No. and Diameter.

Mark Yes or No for Consumable Insert and for Penetration Enhancing Flux, and enter the Deposited Weld Metal Thickness.

Current, transfer mode and shielding gas
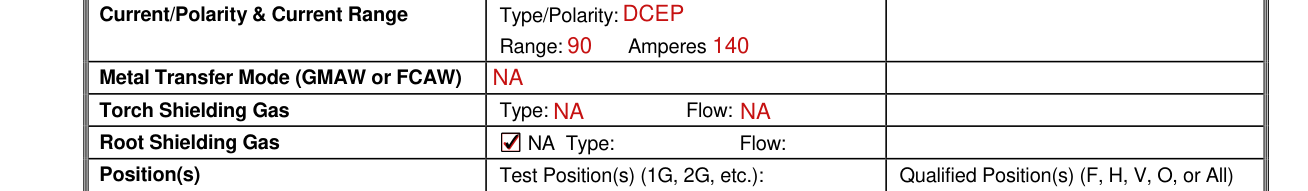
Welder and Welding Operator Performance Qualification Record example filled out, current, transfer mode and shielding gas

Enter the Current/Polarity & Current Range: Type/Polarity and Range in Amperes; enter the Metal Transfer Mode (GMAW or FCAW).

Enter the Torch Shielding Gas Type and Flow; for the Root Shielding Gas, mark NA or enter the Type and Flow.

Test and qualified positions

Welder and Welding Operator Performance Qualification Record example filled out, test and qualified positions

Enter the Test Position(s) (1G, 2G, etc.) and the Qualified Position(s) (F, H, V, O, or All); mark Uphill or Downhill for the Vertical Progression.

Insert NA for Variables that are identified as Non-essential in the Code or Specification used for the Performance Qualification Test.

Mechanical test results
Welder and Welding Operator Performance Qualification Record example filled out, mechanical test results

For Mechanical Test Results, enter the Type And Figure No. and the Results; enter who the Guided mechanical Testing was Conducted By and the Date.

Nondestructive examination results
Welder and Welding Operator Performance Qualification Record example filled out, nondestructive examination results

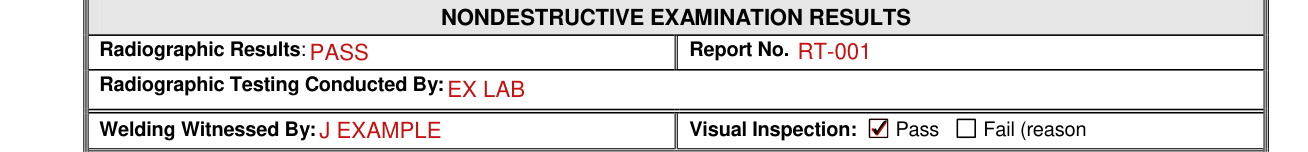
For Nondestructive Examination Results, enter the Radiographic Results and Report No., the Radiographic Testing Conducted By and the Welding Witnessed By; mark Visual Inspection Pass or Fail (reason).

Certification, date qualified and signing

Welder and Welding Operator Performance Qualification Record example filled out, certification, date qualified and signing

The certification states that the statements in this record are correct and the test welds were prepared, welded and tested in accordance with the requirements of: AWS D1.1, AWS B2.1 or Other.

Sign on Signed By with the CWI No., and enter the Date Qualified and the ATF Name and Number.

Sources

[1] Welder and Welding Operator Performance Qualification Record (ATF WPQR Blank Form 2010-04-15) (the Official source link on this page).

Please rate Welder Performance Qualification Record

3 Votes
If you believe this page is infringing on your copyright, please familiarize yourself with and follow our DMCA notice and takedown process - click here to proceed .