How to Fill Out Form QB-484

Form QB-484 at a glance

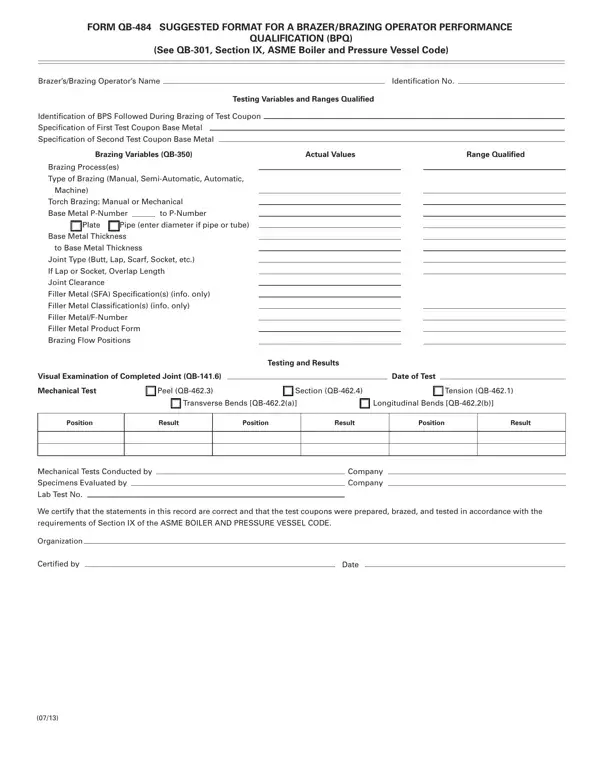
What it is: Form QB-484 is a suggested format for a brazer or brazing operator performance qualification (BPQ), see QB-301, Section IX, ASME Boiler and Pressure Vessel Code.

Who signs: The Organization certifies that the statements in this record are correct, and the Certified by line is for the Organization.

A filled-in Form QB-484 example: a brazer records a tension test
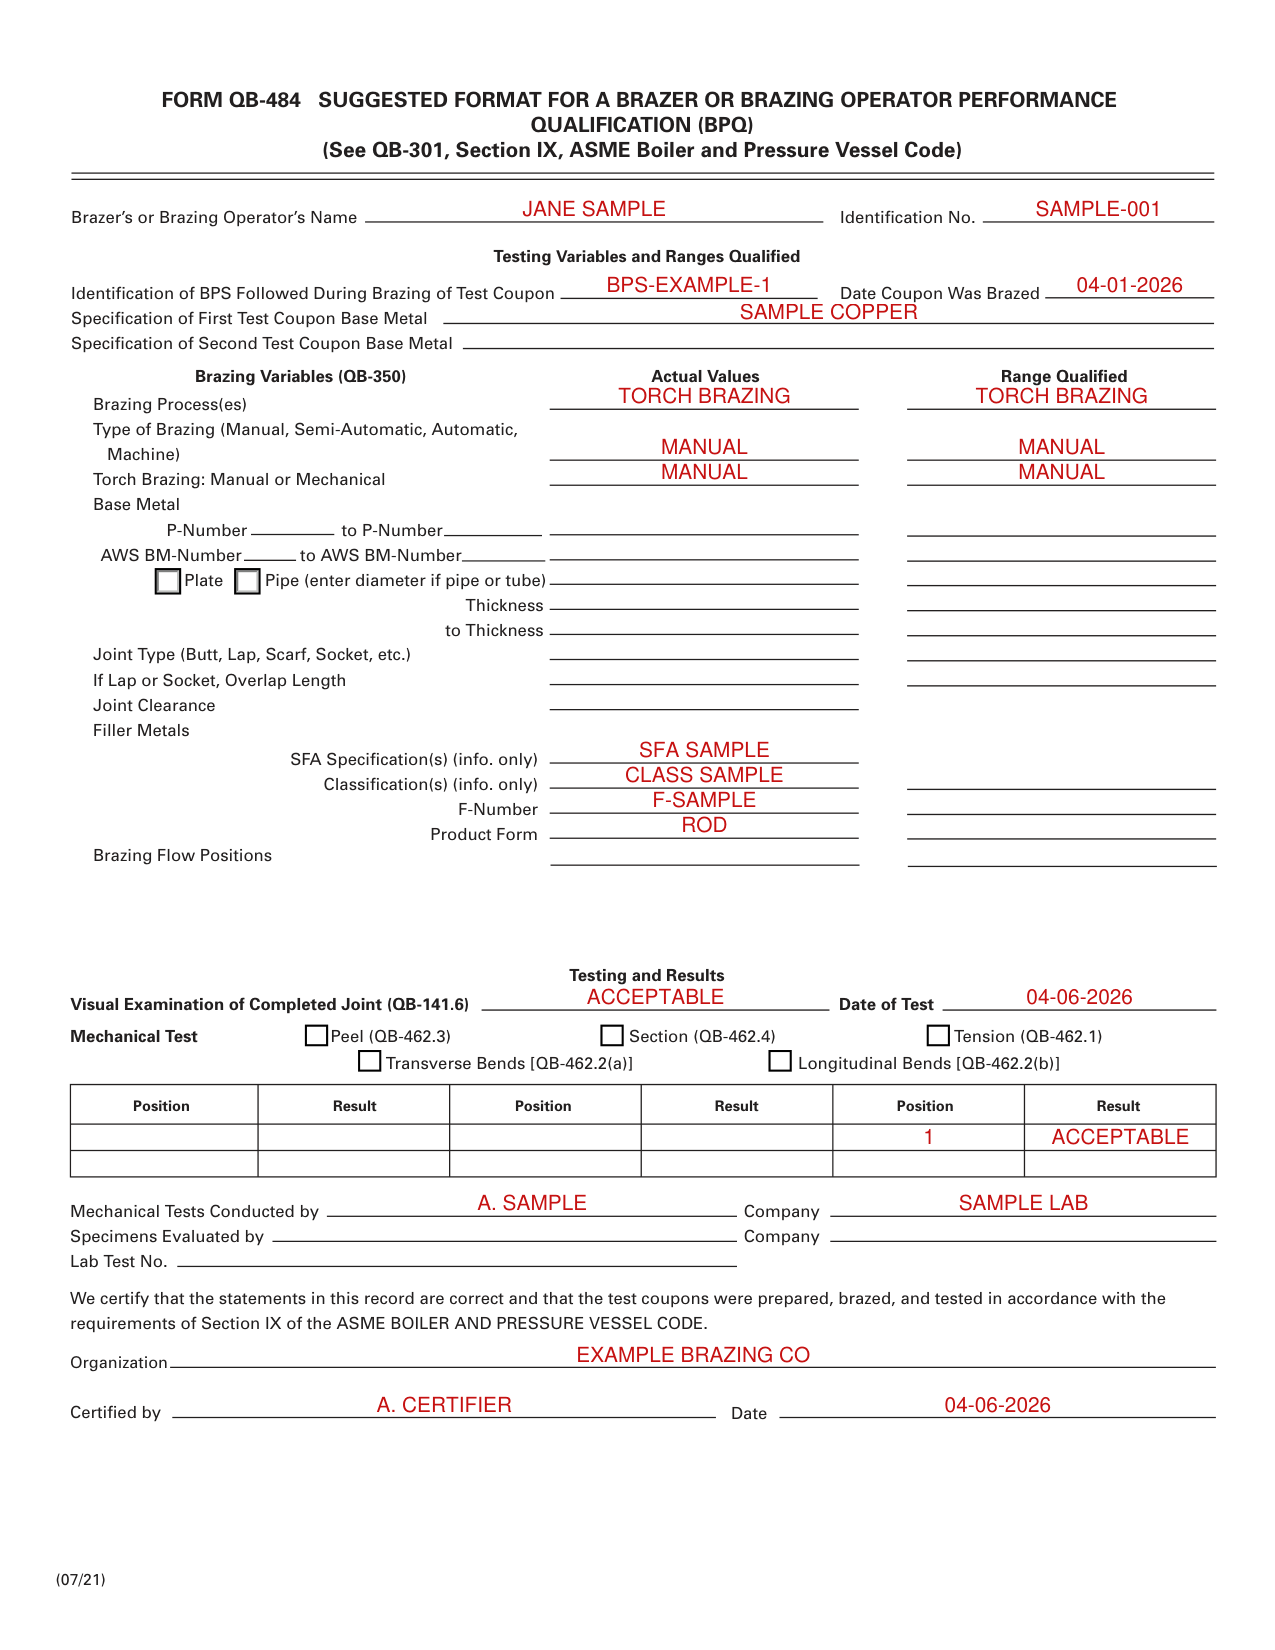
Form QB-484 example filled out, example: a brazer records a tension test
A brazer at a sample shop records hand torch brazing on Form QB-484. Filler metal is used, and the coupon passes visual examination and one tension test on April 6, 2026. Example Brazing Co certifies the record. The picture shows page 1, and its names and figures are sample values.

How to fill out Form QB-484, box by box

Name, identification and the coupon
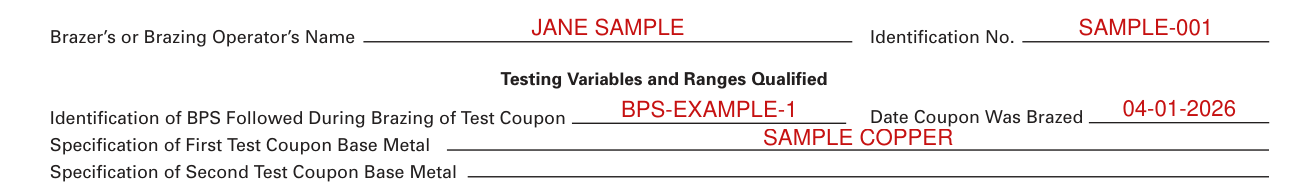
Form QB-484 example filled out, name, identification and the coupon

Enter the Brazer's or Brazing Operator's Name and the Identification No.

Enter the Identification of BPS Followed During Brazing of Test Coupon, the Specification of First Test Coupon Base Metal, the Specification of Second Test Coupon Base Metal and the Date Coupon Was Brazed.

Brazing variables and ranges qualified
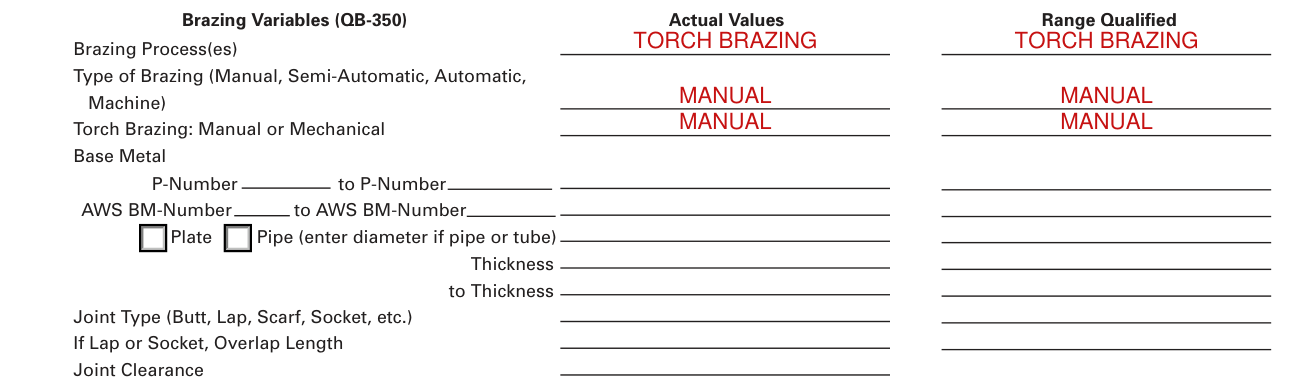
Form QB-484 example filled out, brazing variables and ranges qualified

Under Testing Variables and Ranges Qualified, enter the Actual Values and the Range Qualified for the Brazing Variables (QB-350).

List the Brazing Process(es), the Type of Brazing (Manual, Semi-Automatic, Automatic, Machine) and, for Torch Brazing, Manual or Mechanical.

Enter the P-Number to P-Number and the AWS BM-Number to AWS BM-Number, Plate or Pipe (enter diameter if pipe or tube) and the Thickness to Thickness.

Enter the Joint Type (Butt, Lap, Scarf, Socket, etc.), the Overlap Length if Lap or Socket, and the Joint Clearance.

SFA specifications, F-Number and brazing flow positions
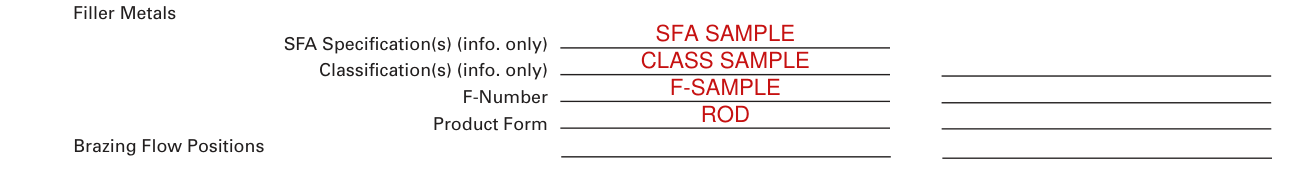
Form QB-484 example filled out, sFA specifications, F-Number and brazing flow positions

Enter the SFA Specification(s) (info. only), the Classification(s) (info. only), the F-Number and the Product Form.

Enter the Brazing Flow Positions.

Testing and results
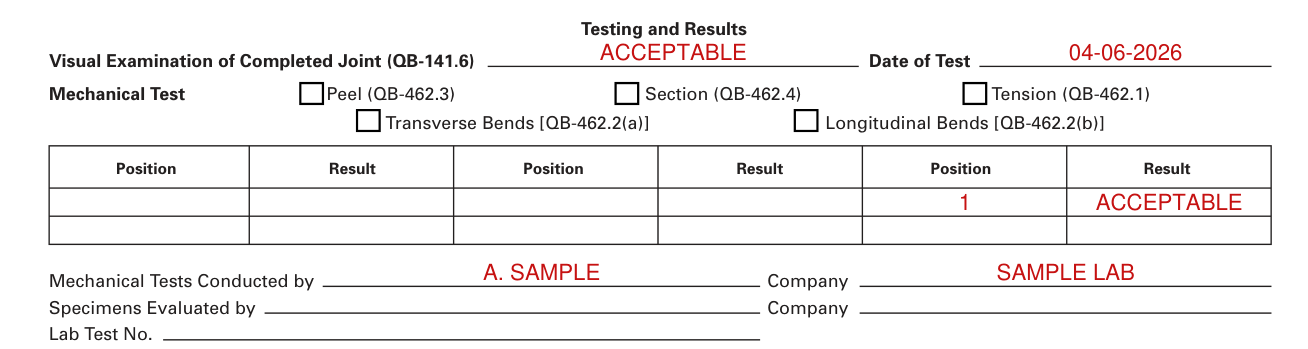
Form QB-484 example filled out, testing and results

Under Testing and Results, enter the Visual Examination of Completed Joint (QB-141.6) and the Date of Test.

Check the Mechanical Test, Peel (QB-462.3), Section (QB-462.4), Tension (QB-462.1), Transverse Bends [QB-462.2(a)] or Longitudinal Bends [QB-462.2(b)], and enter the Position and the Result.

Enter the Mechanical Tests Conducted by and the Company, the Specimens Evaluated by and the Company, and the Lab Test No.

Certification
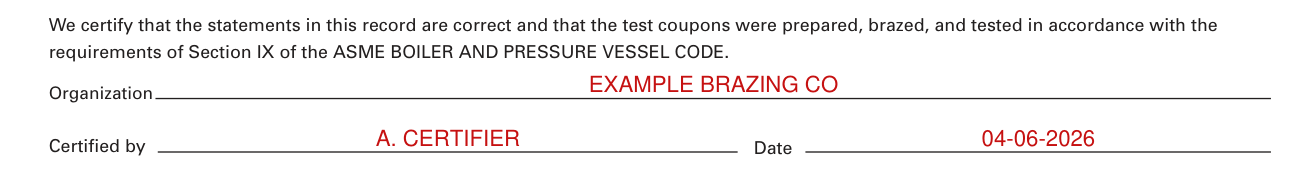
Form QB-484 example filled out, certification

Certify that the statements in this record are correct and that the test coupons were prepared, brazed, and tested in accordance with the requirements of Section IX of the ASME BOILER AND PRESSURE VESSEL CODE.

Enter the Organization, the Certified by and the Date.

Sources

[1] Form QB-484 (07/21), Suggested Format for a Brazer or Brazing Operator Performance Qualification (BPQ), ASME (the Official source link on this page).

Form Qb 484 PDF Details

The QB-484 form serves as a critical document for brazers and brazing operators seeking to verify their qualifications in line with Section IX of the ASME Boiler and Pressure Vessel Code. This comprehensive form helps ensure that individuals operating in these capacities meet the stringent requirements set forth for brazing tasks, specifically in the construction and repair of pressure vessels and boilers. It requires detailed information about the brazer or brazing operator, including their name and identification number. Through the QB-484, one can document various aspects of the brazing procedure, such as the testing variables, identification of the brazing procedure specification (BPS) followed, the specification of base metals used in the test coupons, and the brazing variables according to QB-350, which covers the actual values and the range qualified. Furthermore, this form outlines the brazing process type, whether manual, semi-automatic, automatic, or machine-operated, and covers specifics like torch brazing techniques, base metal P-Numbers, joint types, and required filler metal specifications. The form also demands details on the technical aspects of the brazing operation including joint clearance, filler metal product form, and brazing flow positions. Beyond these procedural details, the QB-484 form captures the results of mechanical tests and visual examinations of the brazed joints, indicating the rigor of evaluation these qualifications entail. By certifying the brazing qualifications through such a detailed and structured format, the QB-484 form plays a pivotal role in maintaining high-quality standards within the industry, ensuring that operators are proficient in their craft and capable of producing work that meets or exceeds the critical safety and durability standards required in the construction and maintenance of pressure vessels and boilers.

QuestionAnswer
Form NameForm Qb 484
Form Length1 page
Fillable?Yes
Fillable fields68
Avg. time to fill out15 sec
Other namesonline brazer, x brazers, brazers forms pdf, form qb 484