


Form QW-483 at a glance
What it is: Form QW-483 is the Suggested Format for Procedure Qualification Records (PQR); see QW-200.2, Section IX, ASME Boiler and Pressure Vessel Code. Record Actual Variables Used to Weld Test Coupon.
Who signs: The Organization certifies that the statements in this record are correct and that the test welds were prepared, welded, and tested in accordance with the requirements of Section IX of the ASME Boiler and Pressure Vessel Code. Enter Tests Conducted by, the Laboratory Test No., the Organization, the Date and Certified by. Detail of record of tests are illustrative only and may be modified to conform to the type and number of tests required by the Code.
A filled-in Form QW-483 example: a welding procedure test record
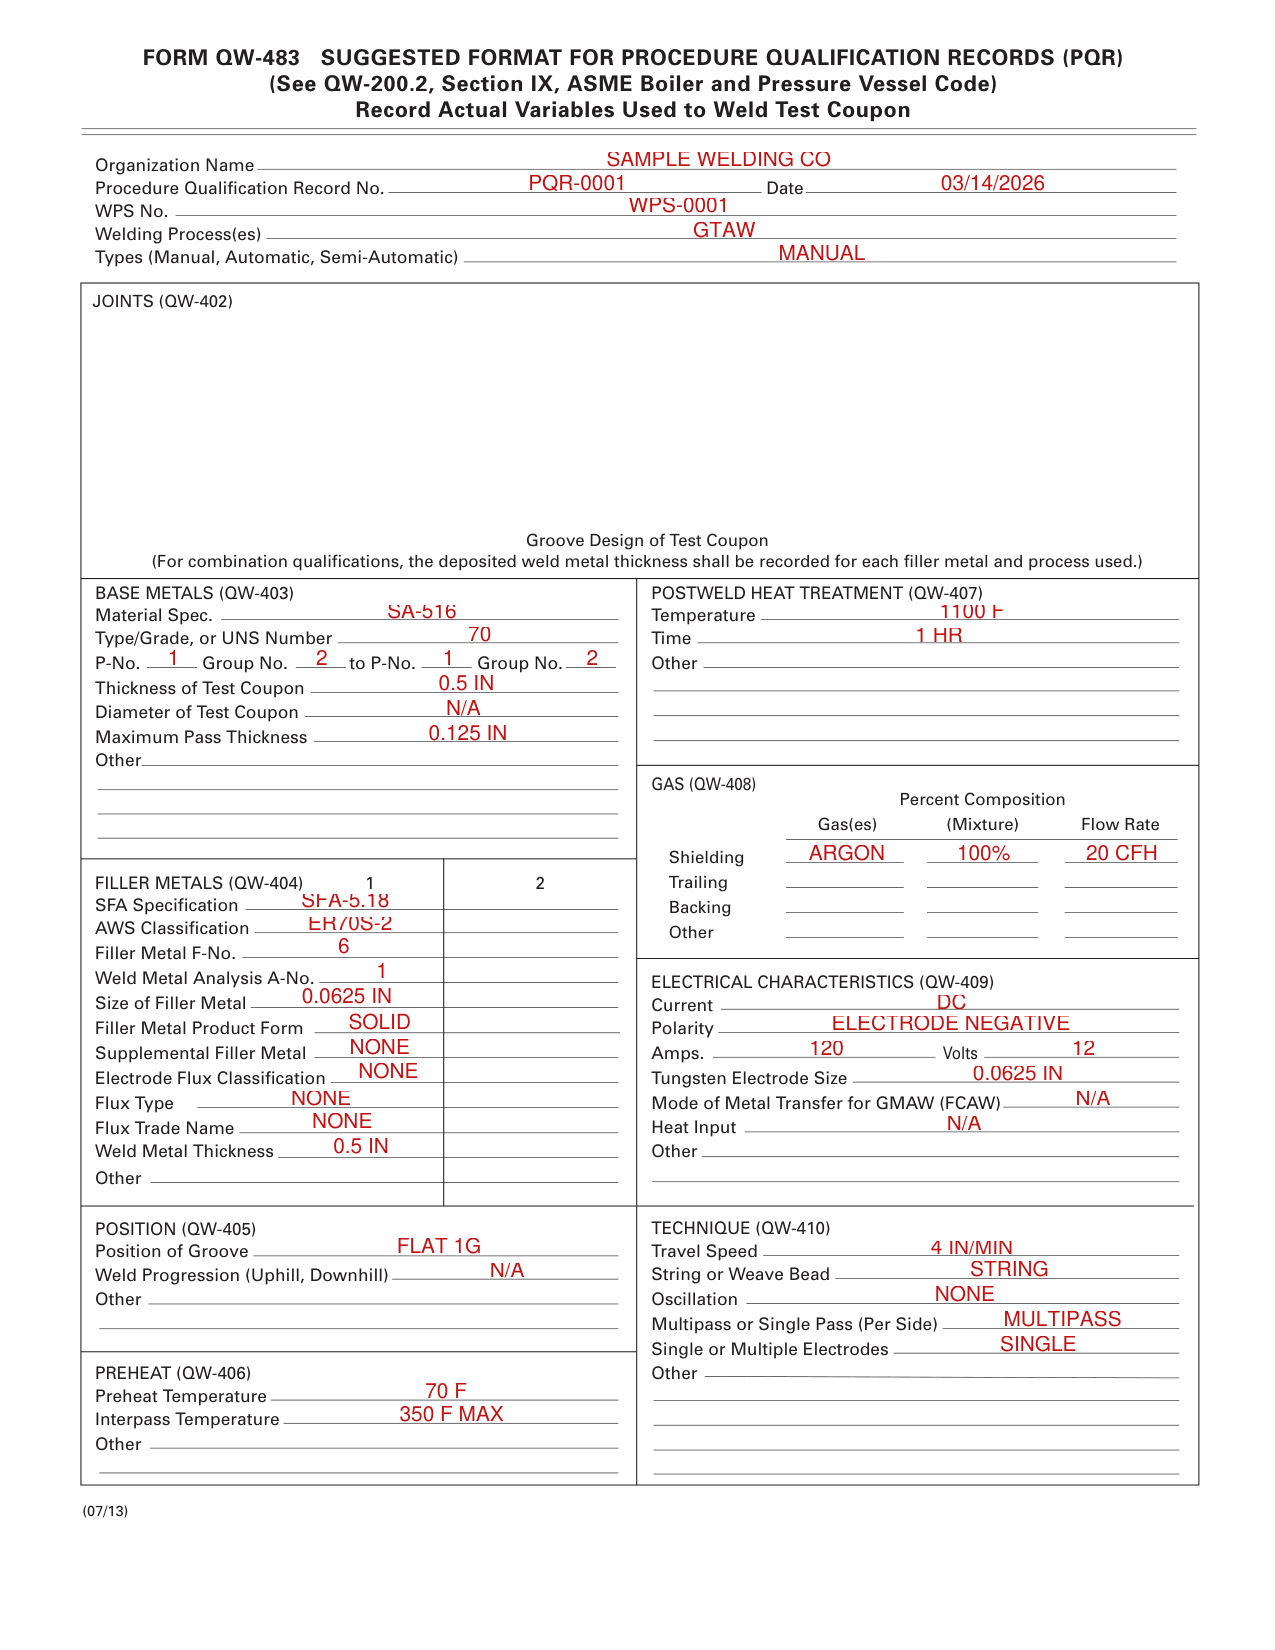
How to fill out Form QW-483, box by box
Organization, record and welding process
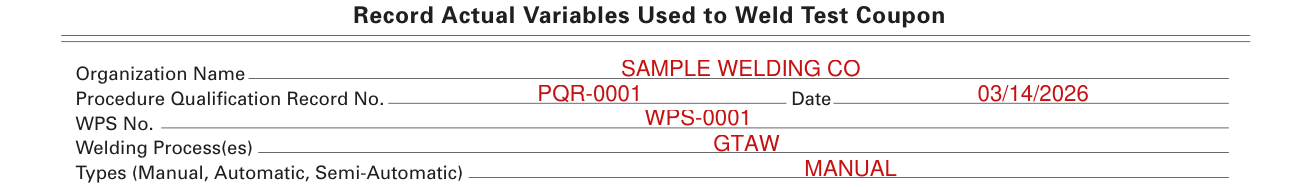
Enter the Organization Name, Procedure Qualification Record No., Date, WPS No. and Welding Process(es).
Enter the Types: Manual, Automatic or Semi-Automatic.
JOINTS (QW-402) and BASE METALS (QW-403)
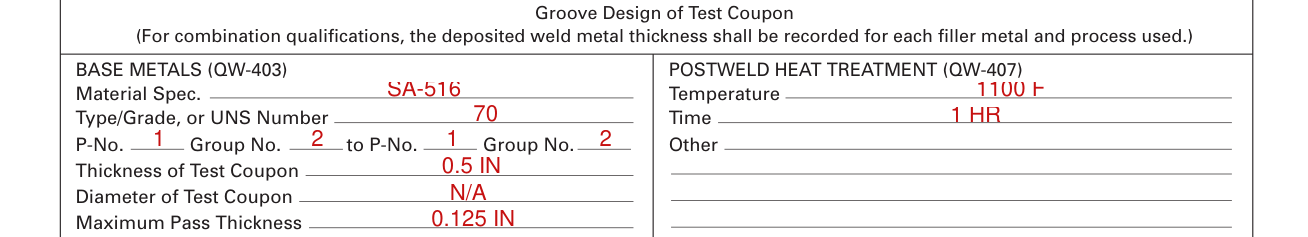
Under JOINTS (QW-402), enter the Groove Design of Test Coupon. For combination qualifications, the deposited weld metal thickness shall be recorded for each filler metal and process used.
Under BASE METALS (QW-403), enter the Material Spec., Type/Grade, or UNS Number, P-No. to P-No., Group No., Thickness of Test Coupon, Diameter of Test Coupon and Maximum Pass Thickness.
POSTWELD HEAT TREATMENT (QW-407)
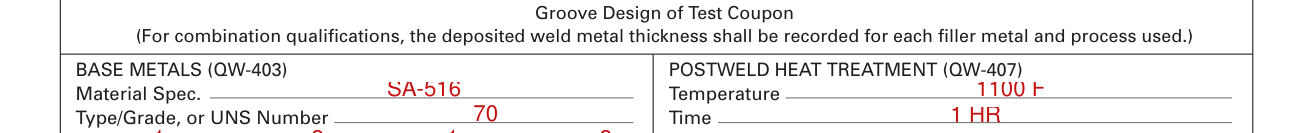
Under POSTWELD HEAT TREATMENT (QW-407), enter the Temperature and Time.
GAS (QW-408)

Under GAS (QW-408), enter the Gas(es), the (Mixture) Percent Composition and the Flow Rate for Shielding, Trailing and Backing.
FILLER METALS (QW-404)
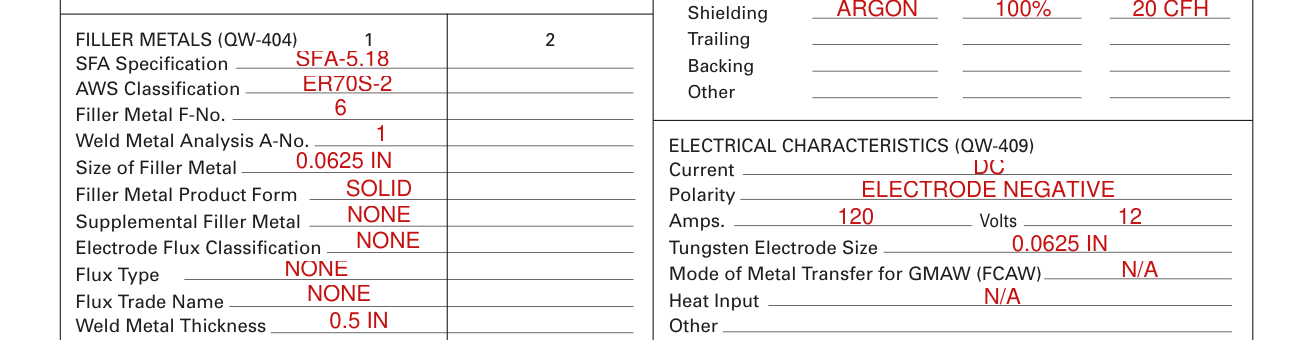
Under FILLER METALS (QW-404), enter for 1 and 2 the SFA Specification, AWS Classification, Filler Metal F-No., Weld Metal Analysis A-No., Size of Filler Metal, Filler Metal Product Form, Supplemental Filler Metal, Electrode Flux Classification, Flux Type, Flux Trade Name and Weld Metal Thickness.
ELECTRICAL CHARACTERISTICS (QW-409)
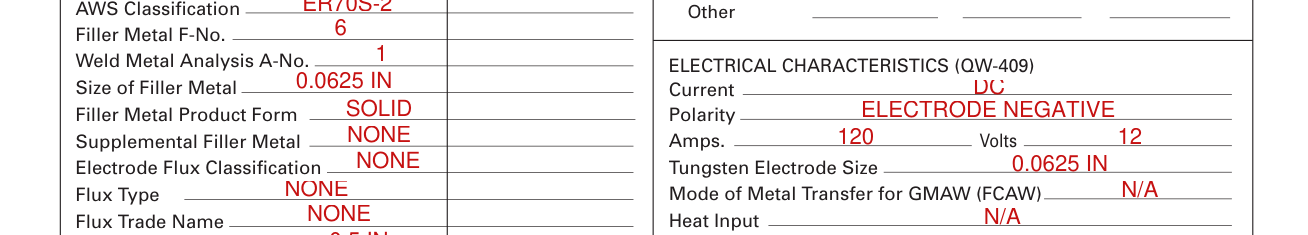
Under ELECTRICAL CHARACTERISTICS (QW-409), enter the Current, Polarity, Amps., Volts, Tungsten Electrode Size, Mode of Metal Transfer for GMAW (FCAW) and Heat Input.
POSITION (QW-405) and TECHNIQUE (QW-410)
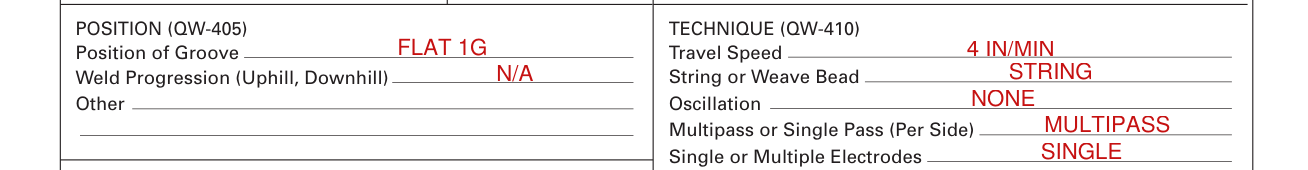
Under POSITION (QW-405), enter the Position of Groove and the Weld Progression (Uphill, Downhill).
Under TECHNIQUE (QW-410), enter the Travel Speed, String or Weave Bead, Oscillation, Multipass or Single Pass (Per Side) and Single or Multiple Electrodes.
PREHEAT (QW-406)

Under PREHEAT (QW-406), enter the Preheat Temperature and the Interpass Temperature.
Tensile Test (QW-150)
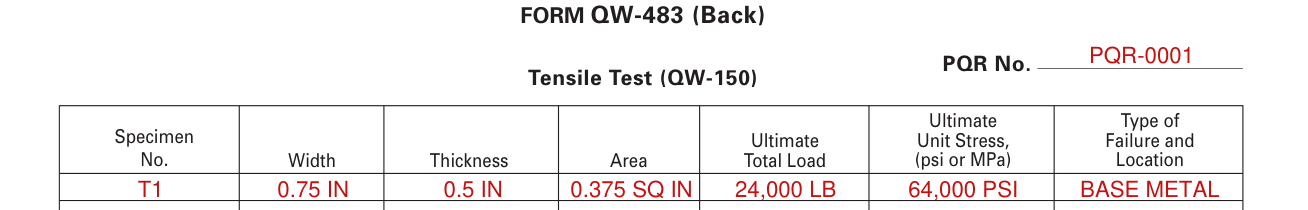
Under Tensile Test (QW-150), enter the PQR No., Specimen No., Width, Thickness, Area, Ultimate Total Load, Ultimate Unit Stress, (psi or MPa), and Type of Failure and Location.
Guided-Bend Tests (QW-160)

Under Guided-Bend Tests (QW-160), enter the Type and Figure No. and the Result.
Fillet-Weld Test (QW-180) and Other Tests
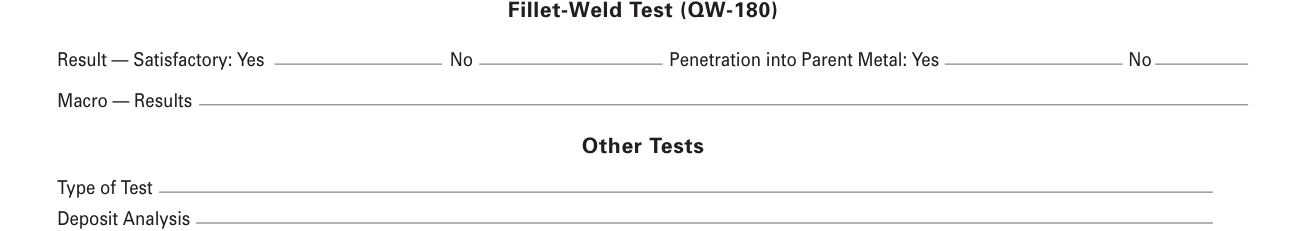
Under Fillet-Weld Test (QW-180), enter the Result - Satisfactory: Yes or No, Penetration into Parent Metal: Yes or No, and Macro - Results.
Under Other Tests, enter the Type of Test and Deposit Analysis.
Welder's name
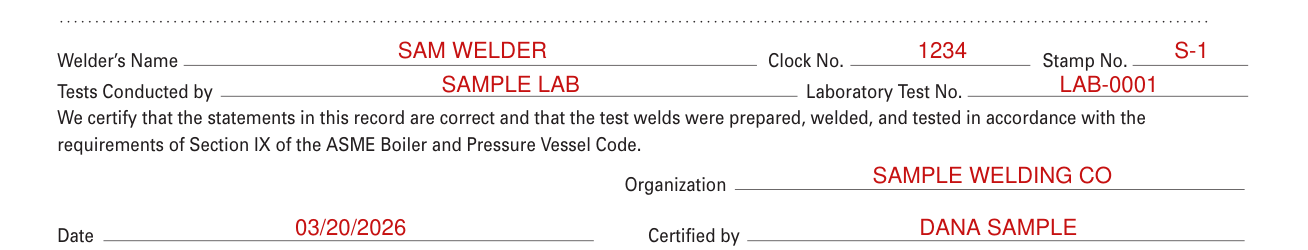
Enter the Welder's Name, Clock No. and Stamp No.
More rules for Form QW-483
Enter the Comments.
Under Toughness Tests (QW-170), enter the Specimen No., Notch Location, Specimen Size, Test Temperature, Impact Values: ft-lb or J, % Shear, Mils (in.) or mm, and Drop Weight Break (Y/N).
Sources
[1] Form QW-483 (07/13), Suggested Format for Procedure Qualification Records (PQR), ASME Boiler and Pressure Vessel Code, Section IX (the served file; no issuer file) (the Official source link on this page).