
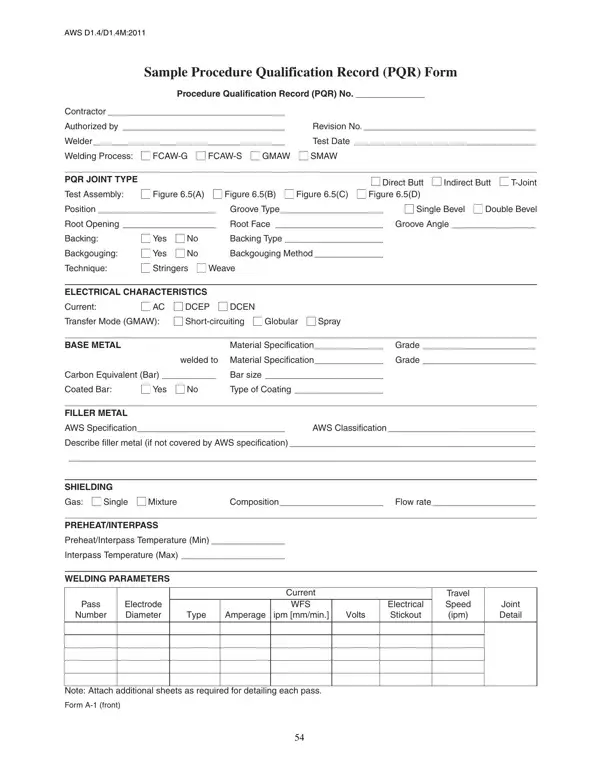

Sample Procedure Qualification Record (PQR) Form at a glance
What it is: Sample Procedure Qualification Record (PQR) Form, Annex A of AWS D1.4/D1.4M:2018-AMD1.
Who signs: Enter the Manufacturer or Contractor, Authorized by and the Date.
The undersigned certify that the statements in this record are correct and that the welds were prepared and tested in accordance with the requirements of AWS D1.4/D1.4M:2018, Structural Welding Code-Steel Reinforcing Bars.
A filled-in Sample Procedure Qualification Record (PQR) Form example: a contractor records a GMAW test
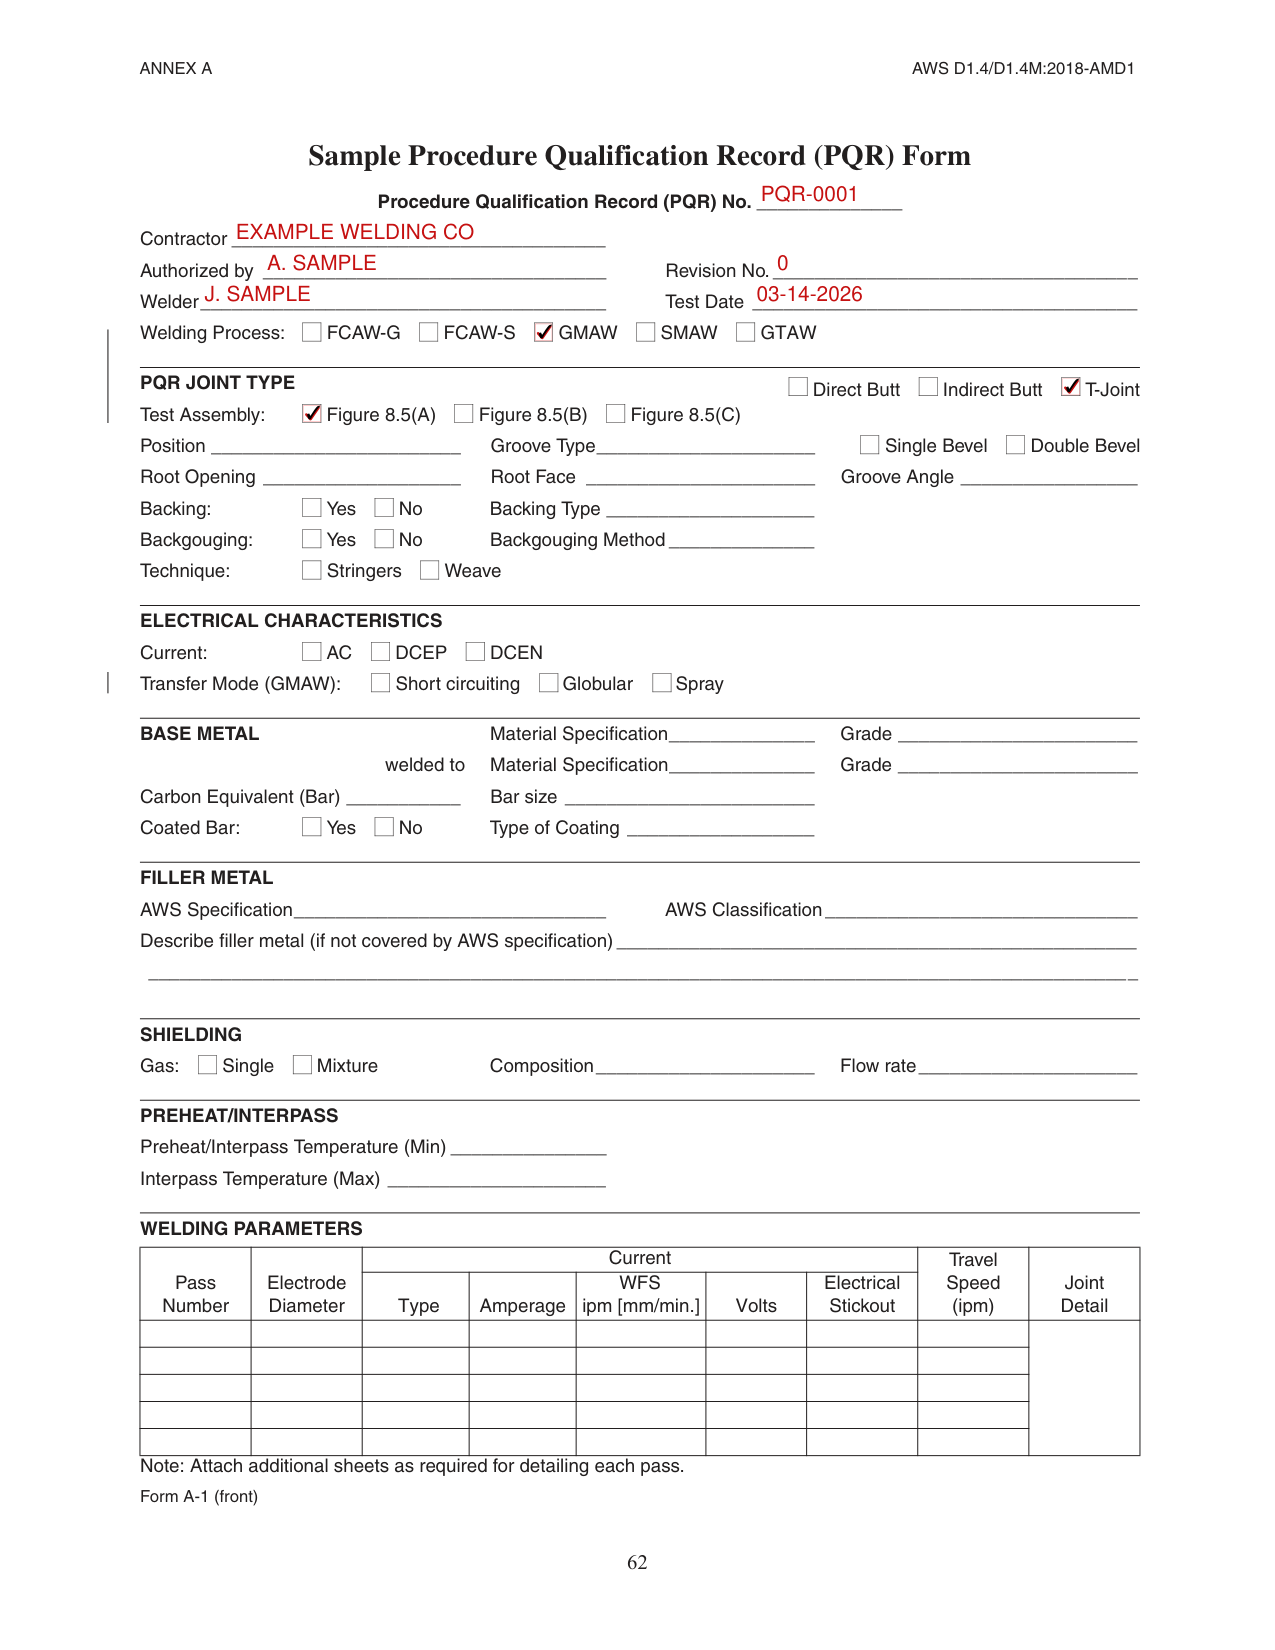
How to fill out Sample Procedure Qualification Record (PQR) Form, box by box
Contractor, welder and welding process
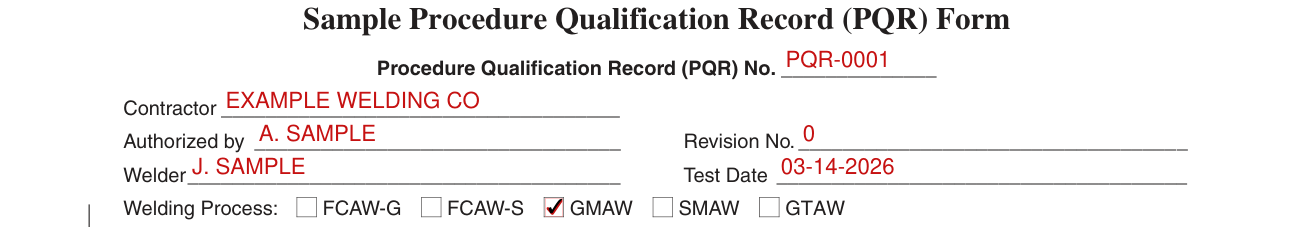
Enter the Procedure Qualification Record (PQR) No., the Contractor, Authorized by, the Revision No., the Welder and the Test Date.
Under Welding Process, mark FCAW-G, FCAW-S, GMAW, SMAW or GTAW.
PQR joint type and groove
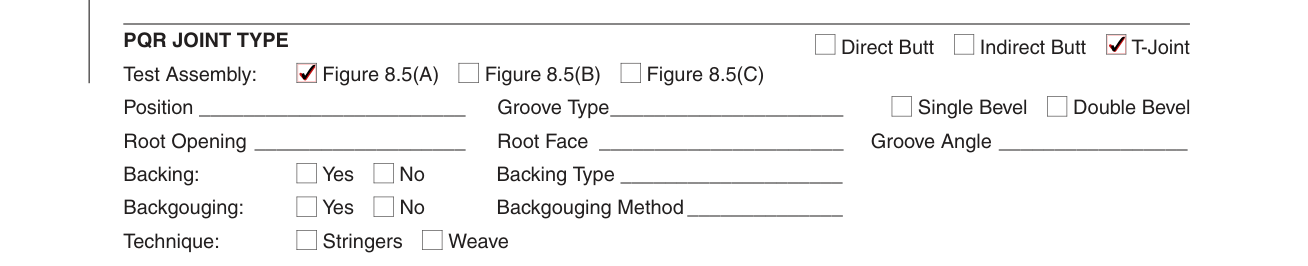
Under PQR JOINT TYPE, mark Direct Butt, Indirect Butt or T-Joint, and mark the Test Assembly: Figure 8.5(A), Figure 8.5(B) or Figure 8.5(C).
Enter the Position, the Groove Type, the Root Opening, the Root Face and the Groove Angle; mark Single Bevel or Double Bevel.
Mark Yes or No for Backing, with the Backing Type, and mark Yes or No for Backgouging, with the Backgouging Method.
Mark the Technique: Stringers or Weave. Mark the Current: AC, DCEP or DCEN. For GMAW, mark the Transfer Mode: Short circuiting, Globular or Spray.
Base metal, filler metal and shielding
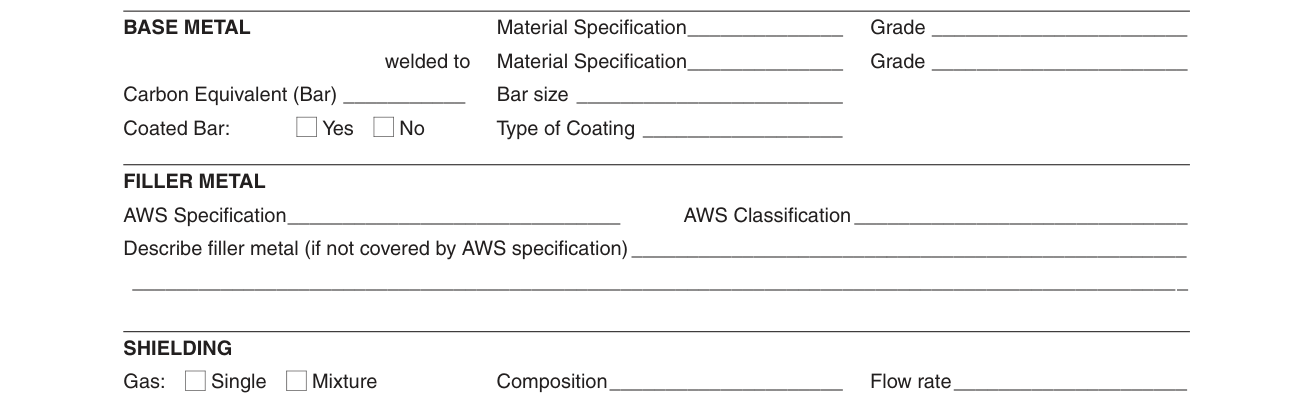
Under BASE METAL, enter the Material Specification and Grade, then the Material Specification and Grade for the metal it is welded to, the Carbon Equivalent (Bar) and the Bar size. Mark Yes or No for Coated Bar and enter the Type of Coating.
Under FILLER METAL, enter the AWS Specification and AWS Classification. Describe the filler metal if it is not covered by an AWS specification.
Under SHIELDING, mark the Gas as Single or Mixture, and enter the Composition and the Flow rate.
Preheat and welding parameters
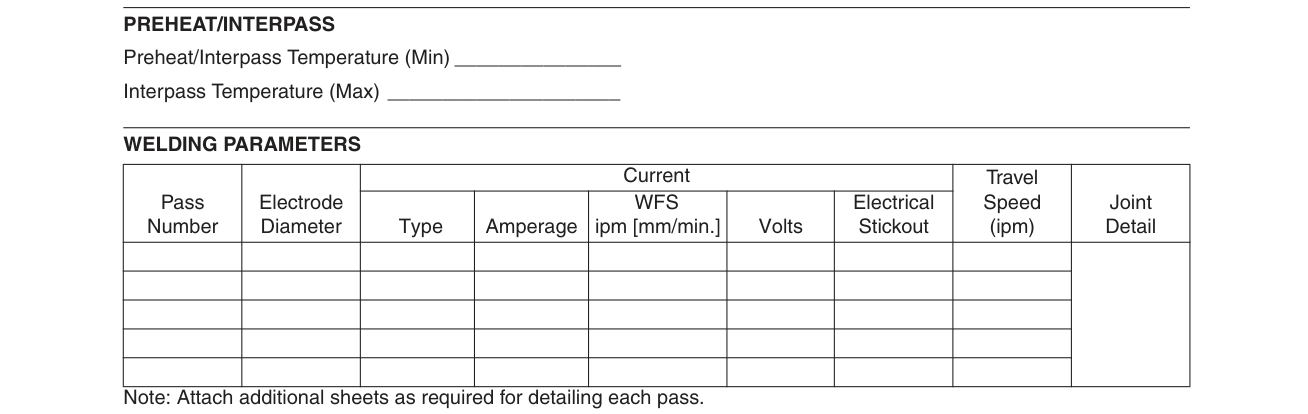
Under PREHEAT/INTERPASS, enter the Preheat/Interpass Temperature (Min) and the Interpass Temperature (Max).
Under WELDING PARAMETERS, for each pass enter the Pass Number, Electrode Diameter, Current Type, Amperage, WFS ipm [mm/min.], Volts, Electrical Stickout, Travel Speed (ipm) and Joint Detail.
Attach additional sheets as required for detailing each pass.
Visual, tensile and macroetch tests
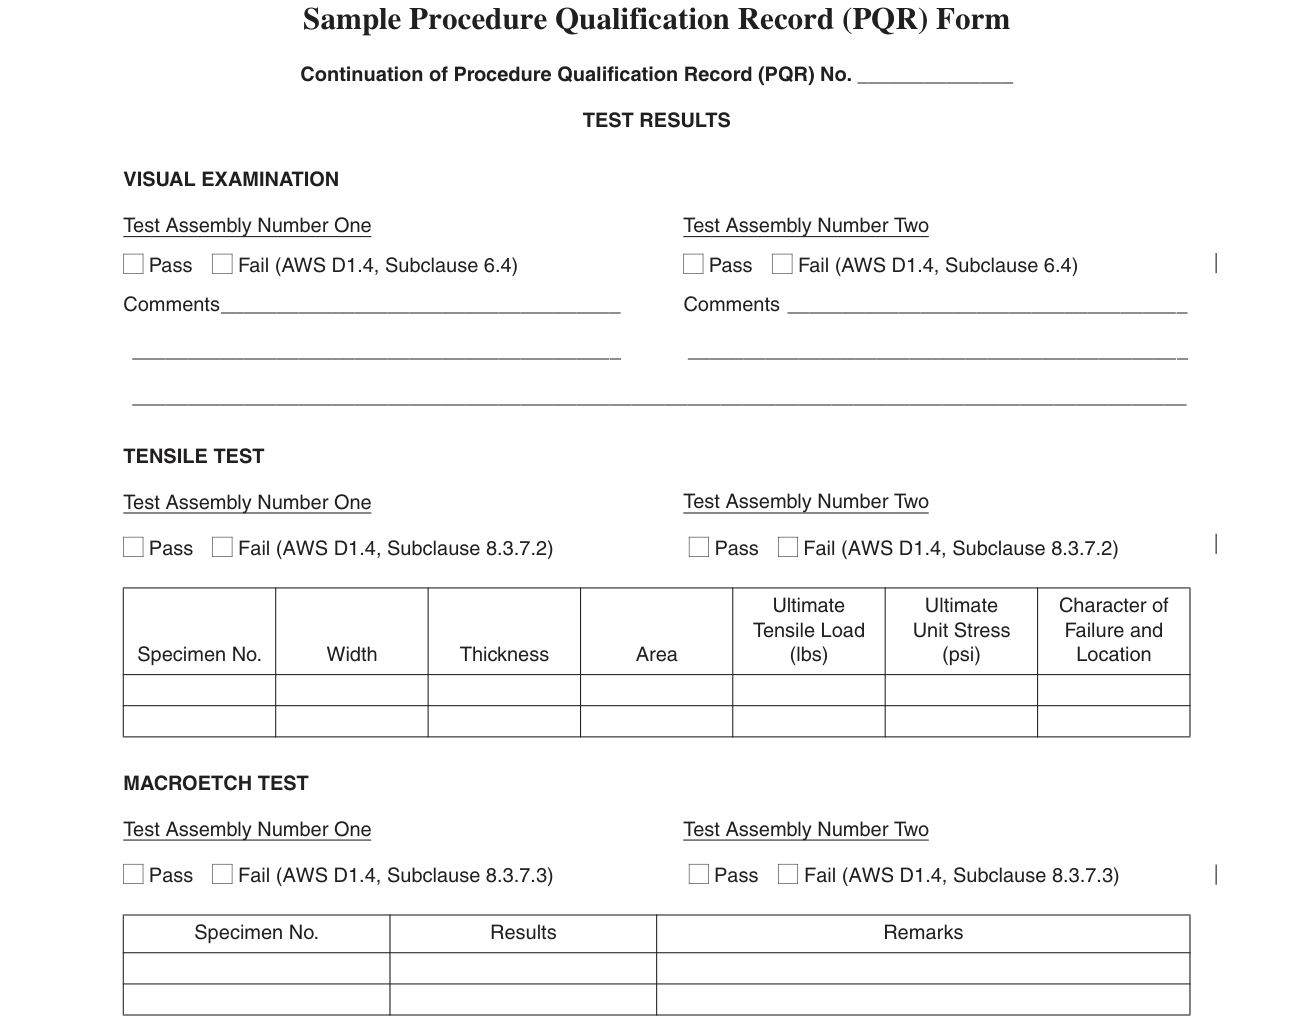
On the continuation page, enter the Procedure Qualification Record (PQR) No.
Under VISUAL EXAMINATION, for Test Assembly Number One and Test Assembly Number Two, mark Pass or Fail (AWS D1.4, Subclause 6.4) and enter Comments.
Under TENSILE TEST, for Test Assembly Number One and Test Assembly Number Two, mark Pass or Fail (AWS D1.4, Subclause 8.3.7.2).
For each tensile specimen, enter the Specimen No., Width, Thickness, Area, Ultimate Tensile Load (lbs), Ultimate Unit Stress (psi) and Character of Failure and Location.
Under MACROETCH TEST, for Test Assembly Number One and Test Assembly Number Two, mark Pass or Fail (AWS D1.4, Subclause 8.3.7.3).
Laboratory, welder and Manufacturer or Contractor
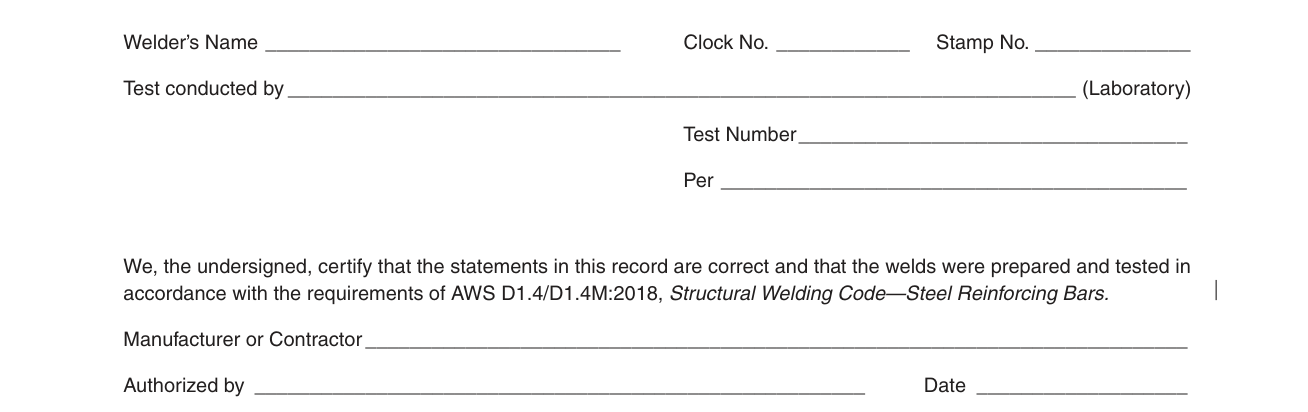
Enter the Welder's Name, Clock No. and Stamp No.; Test conducted by (Laboratory); the Test Number; and Per.
Enter the Manufacturer or Contractor, Authorized by and the Date.
Sources
[1] Sample Procedure Qualification Record (PQR) Form, Annex A, AWS D1.4/D1.4M:2018-AMD1 (the Official source link on this page).